Projects
Real Problems. Proven Results.
Industrial challenges solved across pulp & paper, marine, power plants and more.
Case Study
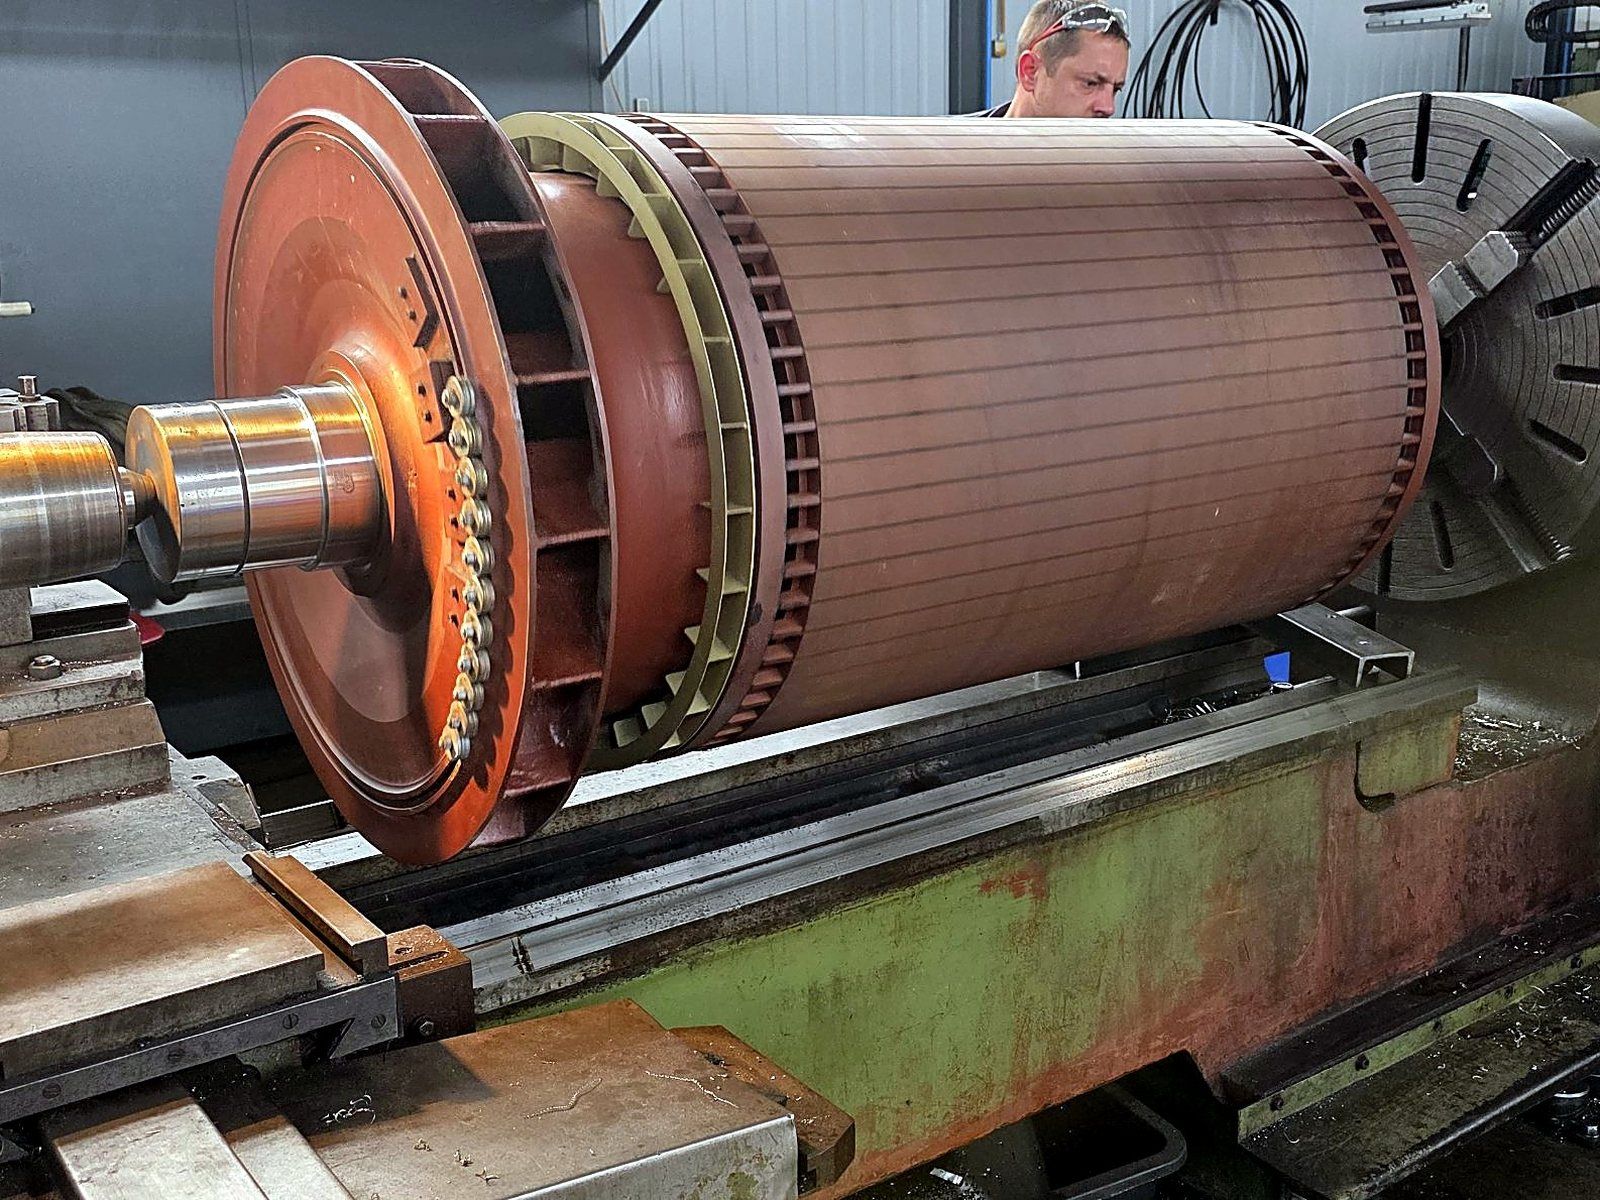
The worn bearing seats were restored and machined back to their original dimensions. The rotor was returned to the customer for assembly two days after it arrived at our workshop. Client: Finland.
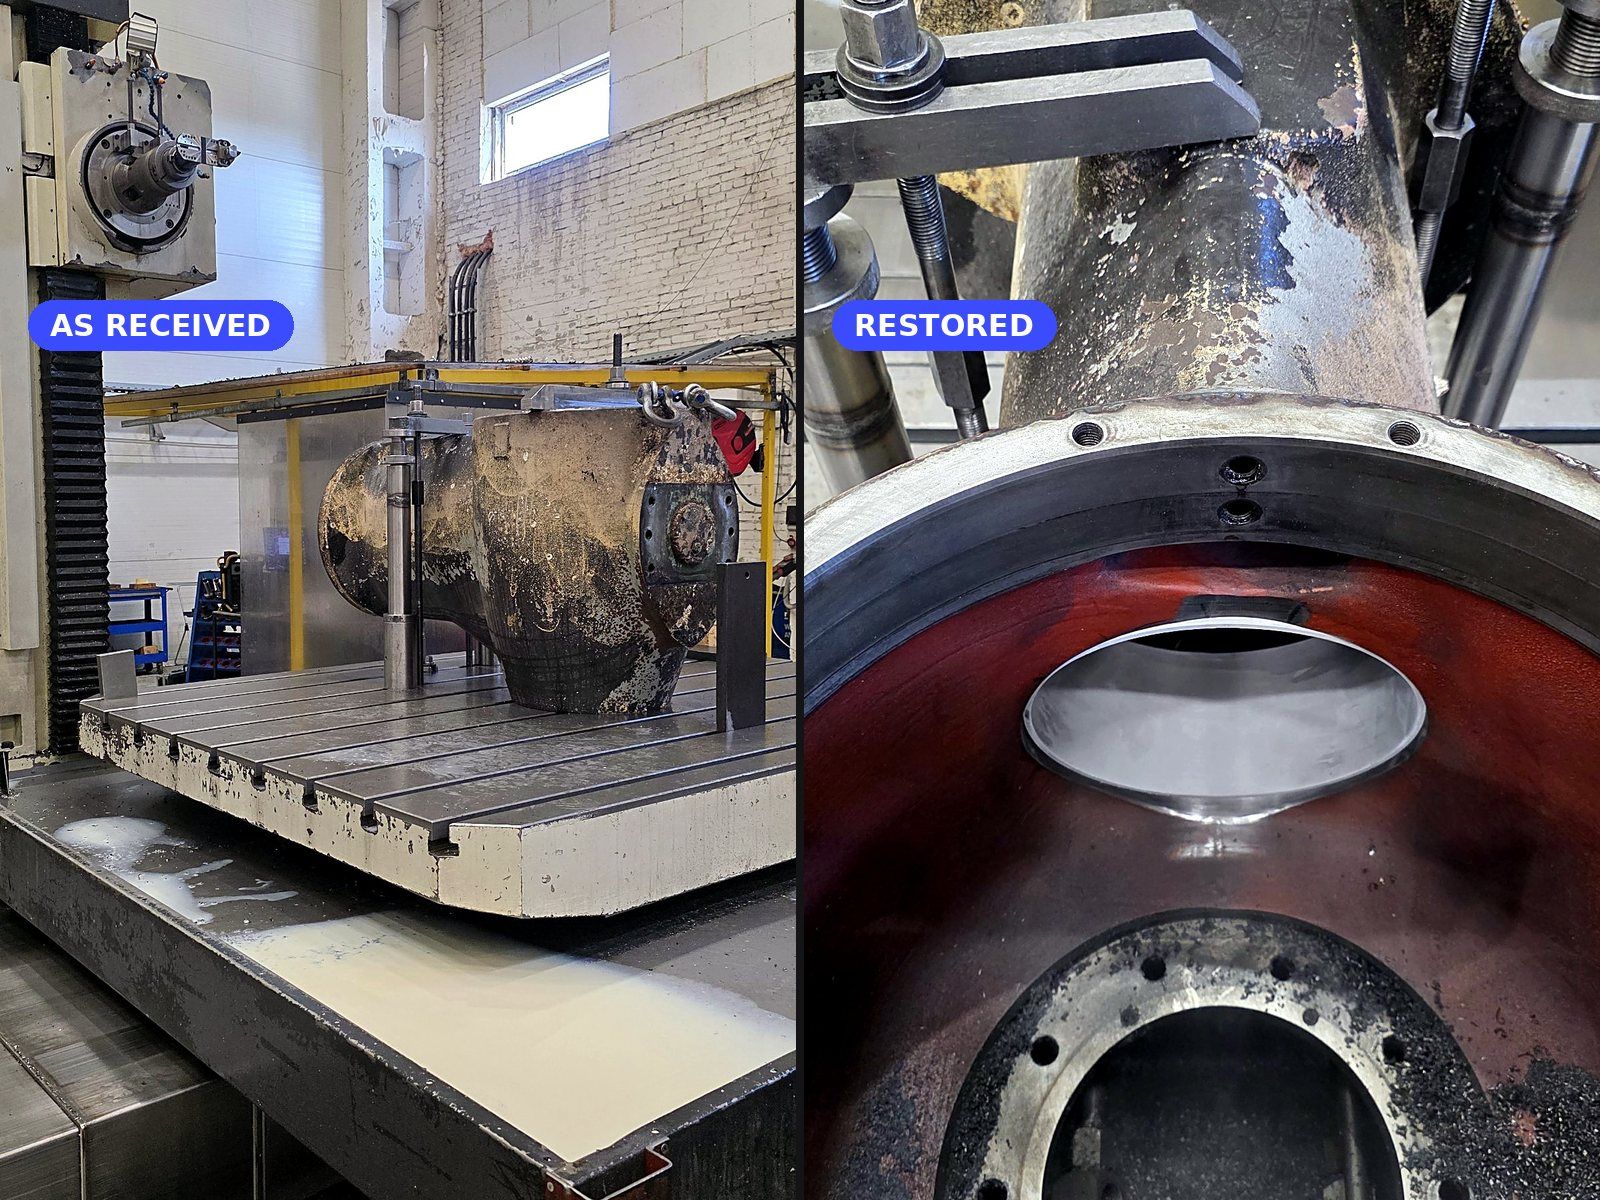
The housing was set up on our horizontal boring mill, where the bearing seat was restored and the housing geometry brought back to original. Client: Norway.
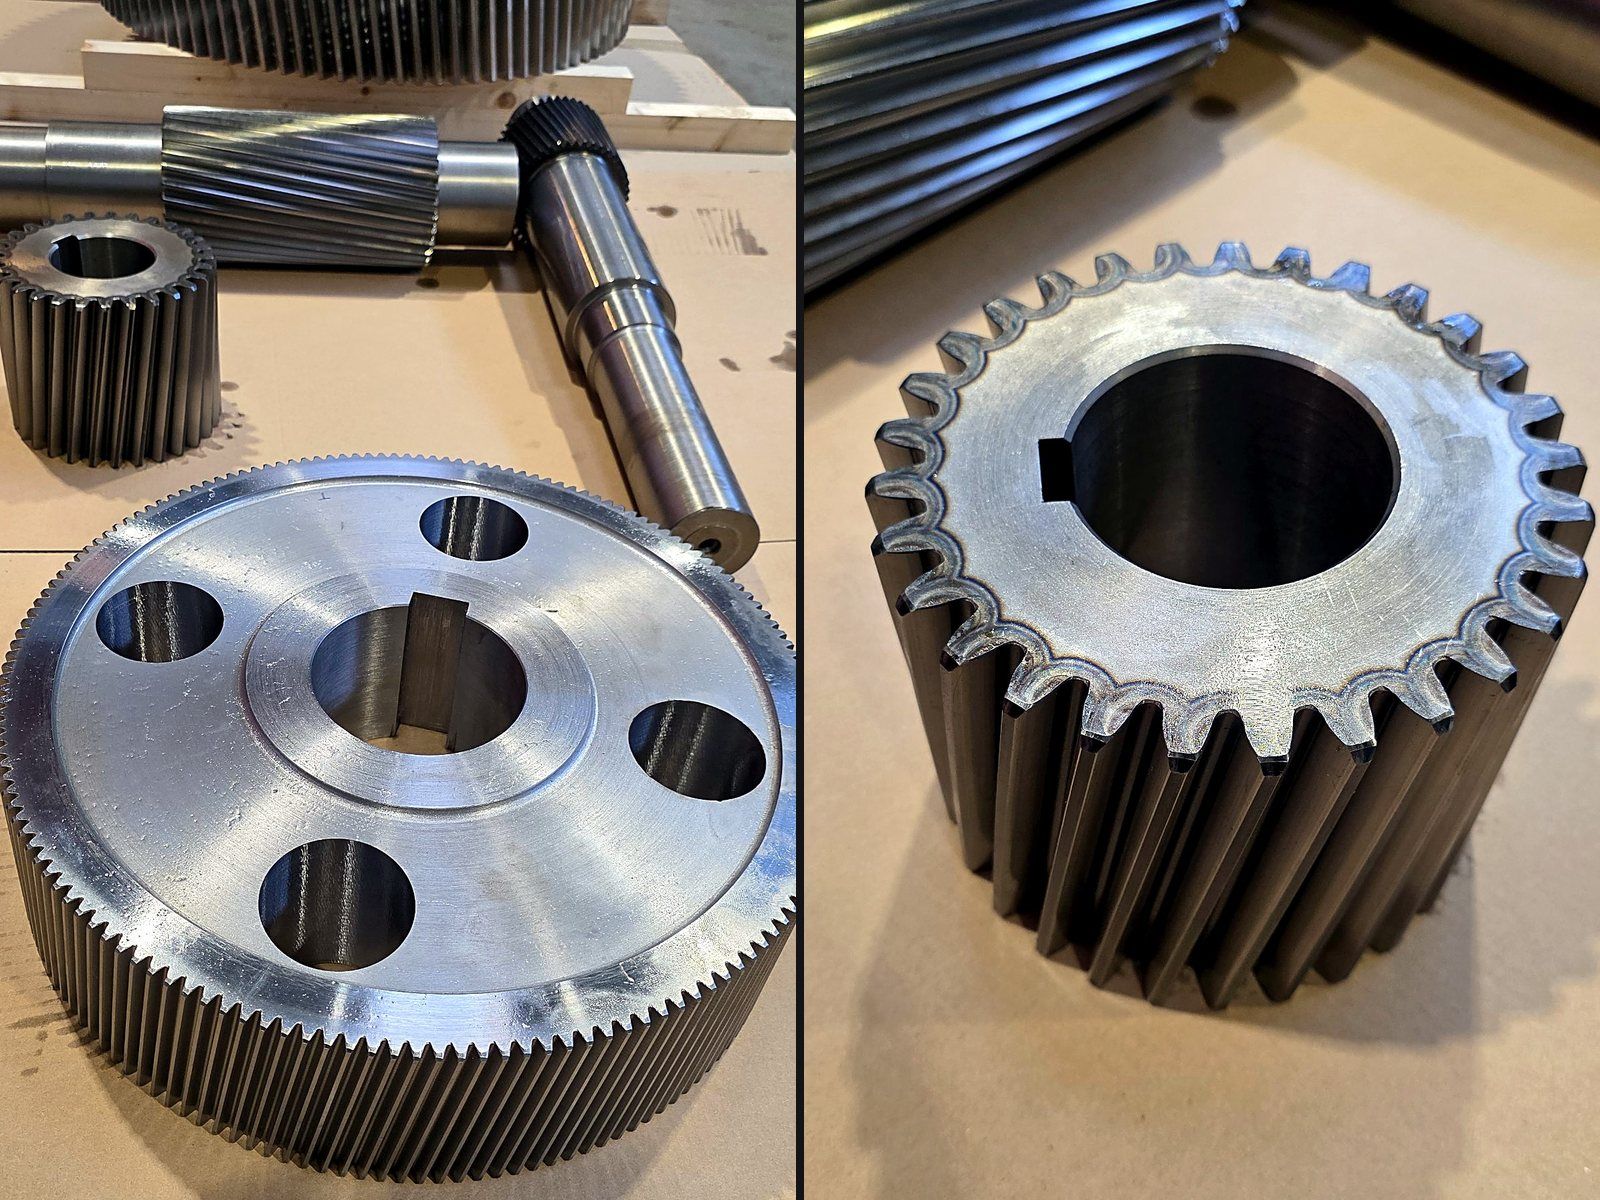
We manufacture spur and helical gears, pinion shafts and gear rings for thrusters, gearboxes, winches and other mechanisms. Client: Norway.
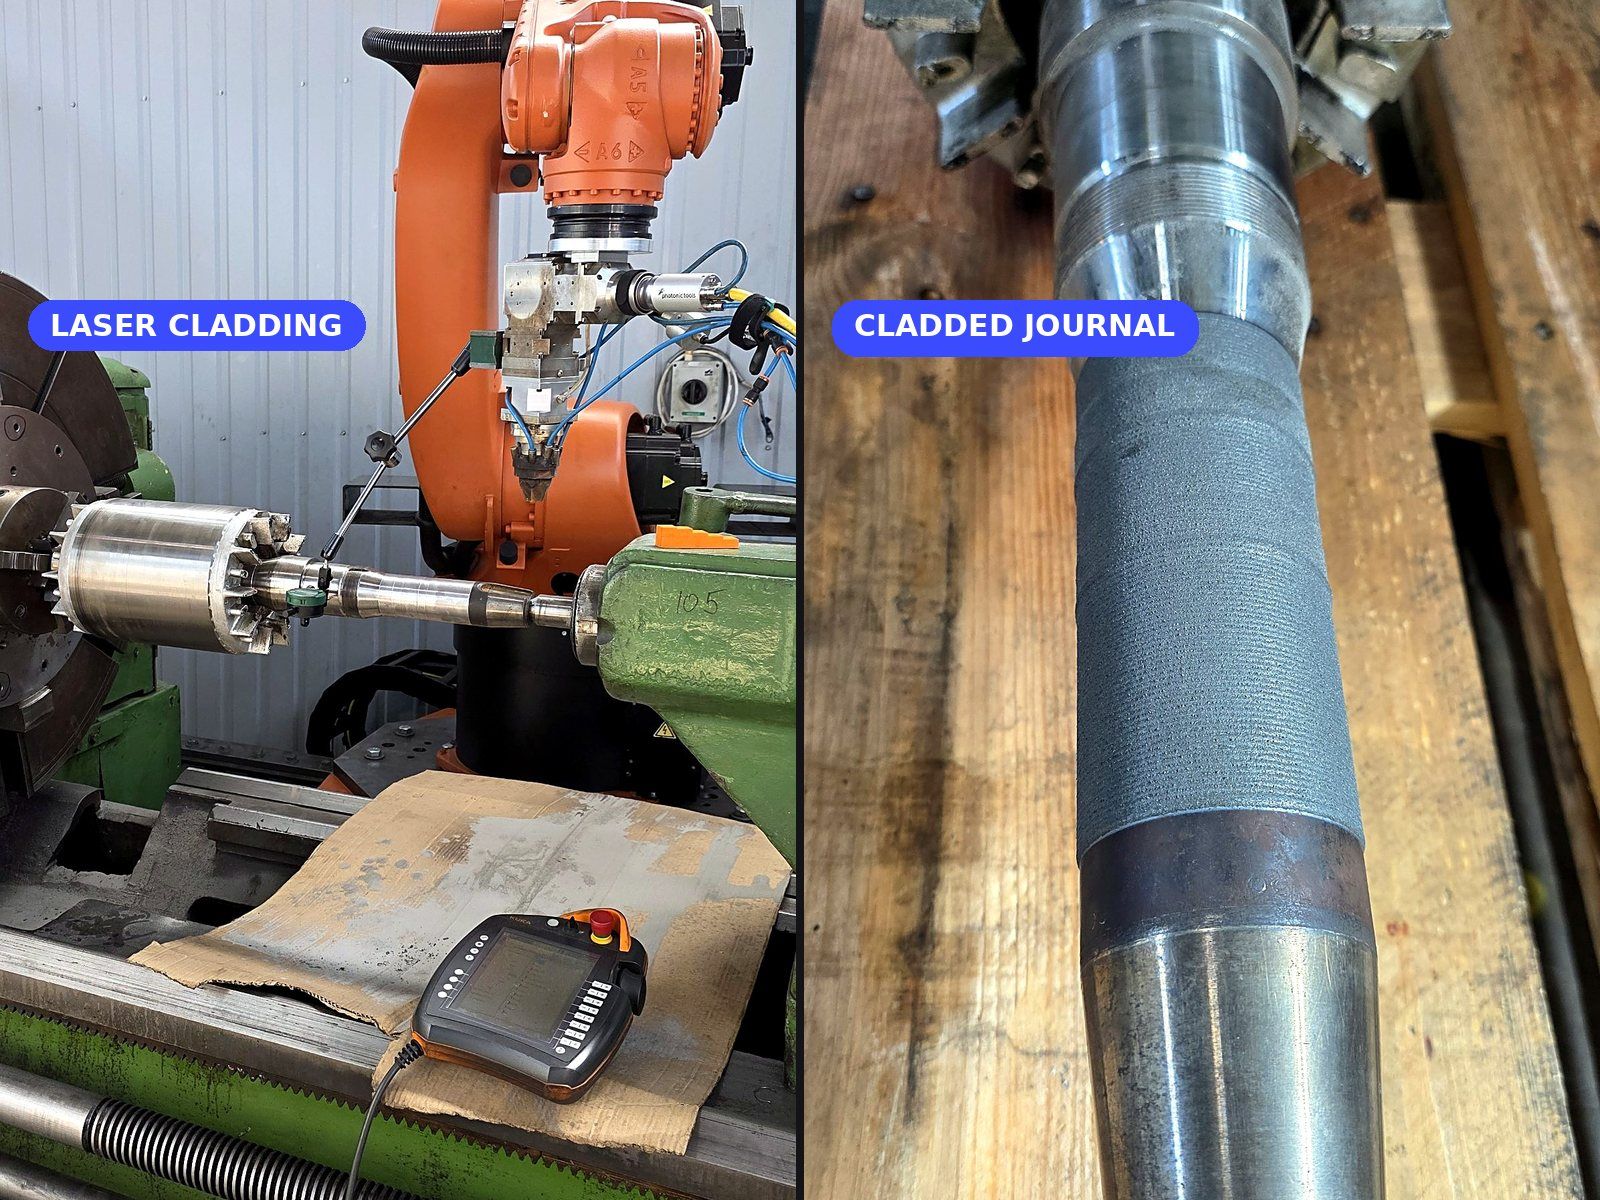
The worn journal was built up by robotic laser cladding and machined back to its original dimensions. Client: Estonia.
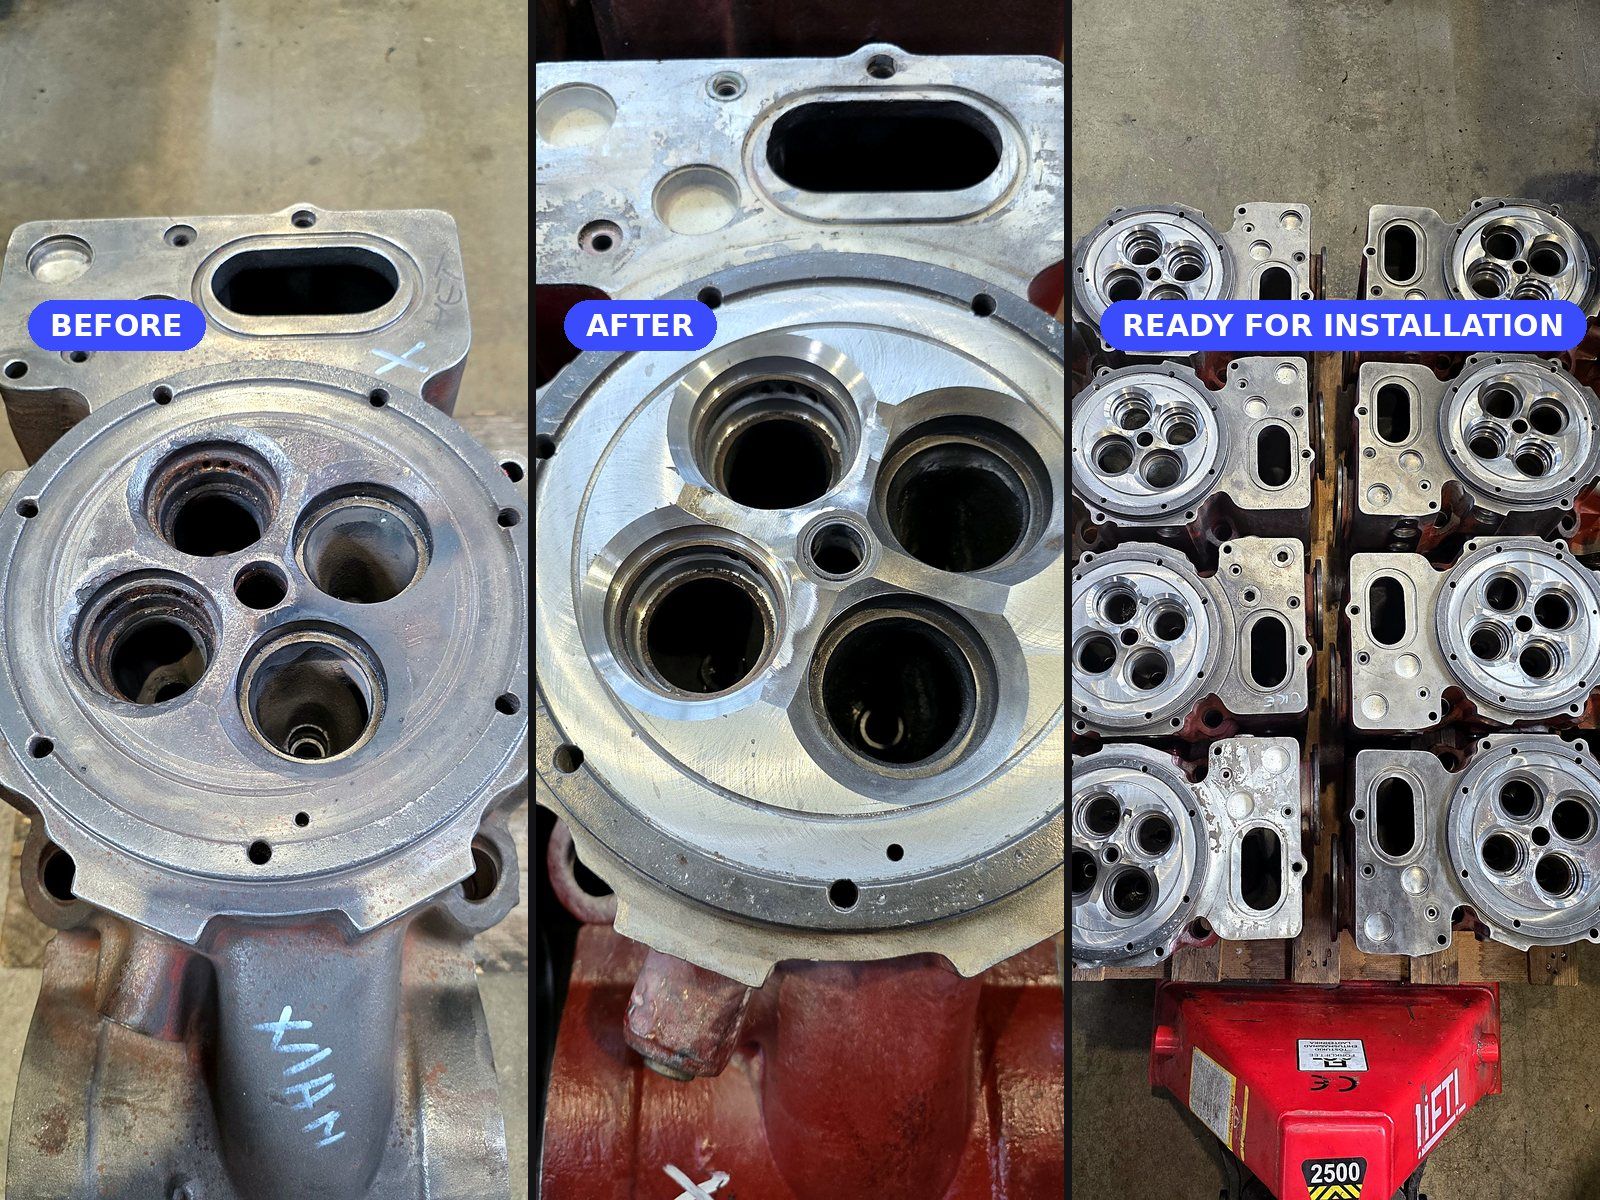
Each exhaust seat pocket was laser clad with 316L stainless steel and machined back to original dimensions. The heads were then assembled and pressure-tested, so the customer received them ready for installation. Client: Finland.
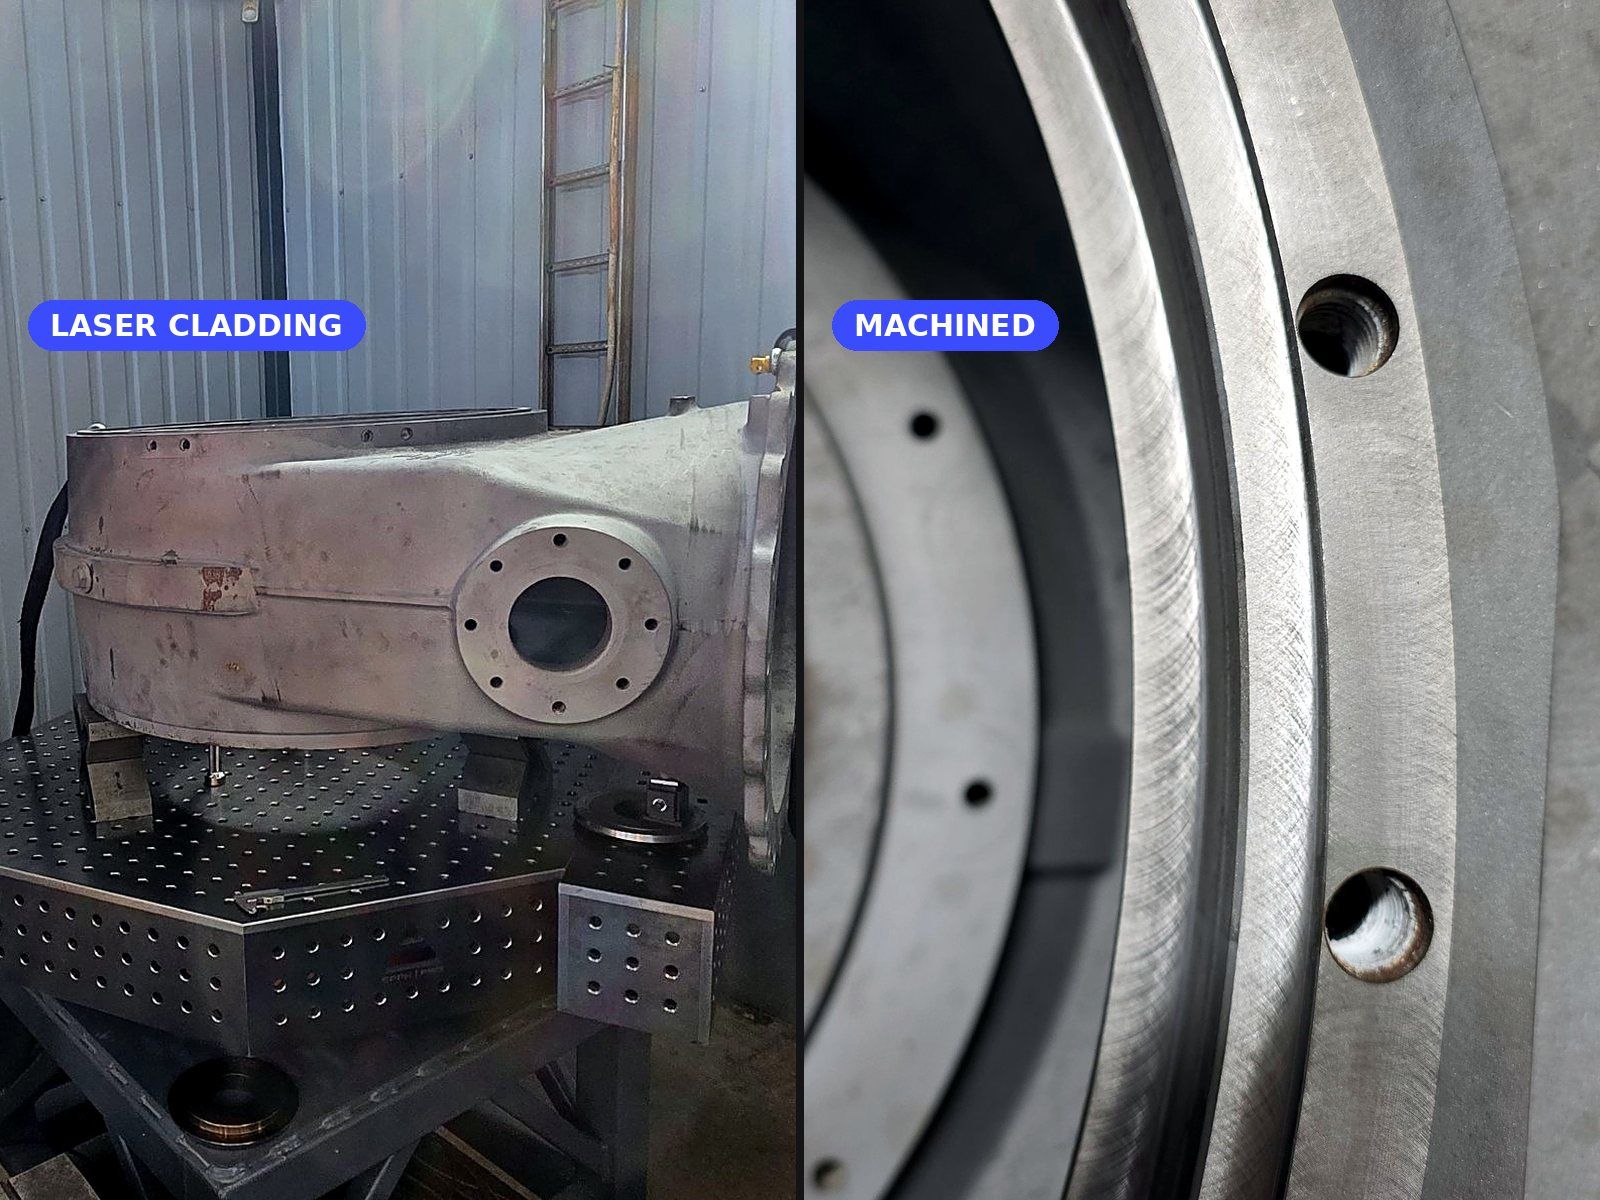
The casing was delivered to our workshop, dismantled and glass-bead blasted. Worn areas were restored by robotic laser cladding and the casing was machined back to its original geometry. Client: Germany.
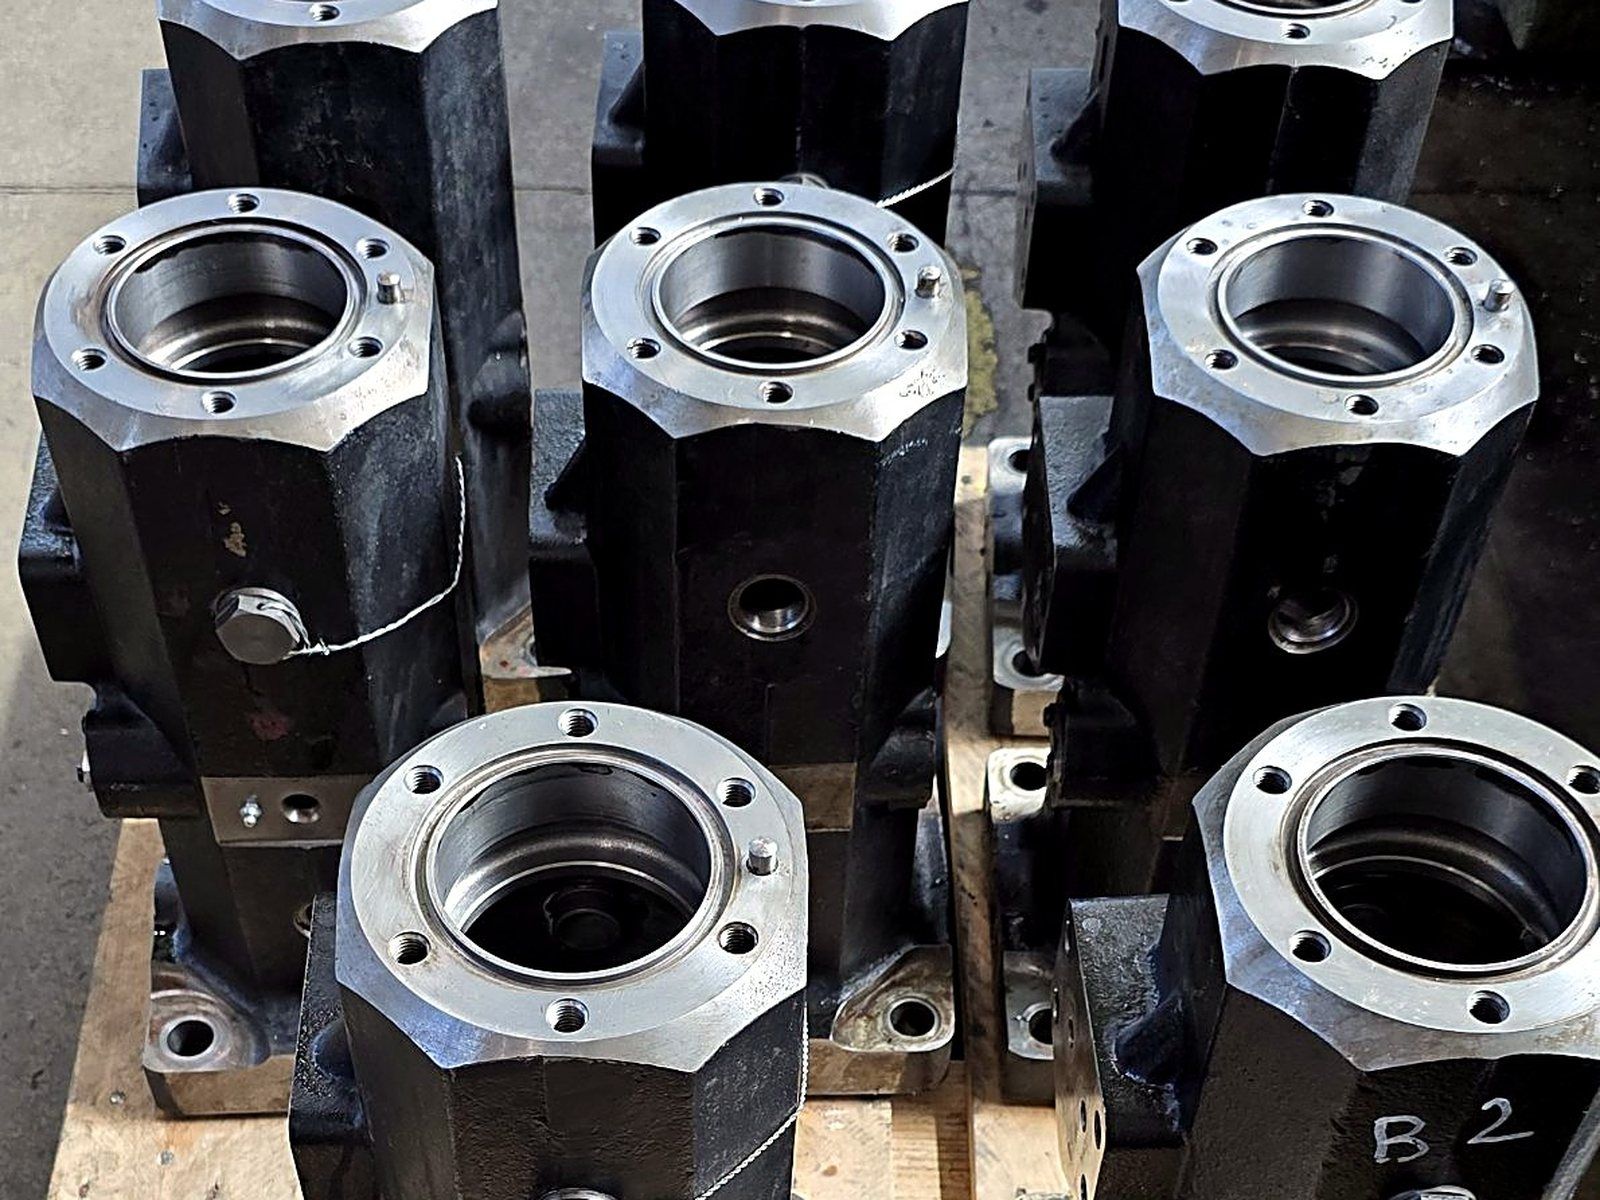
Instead of buying new housings, the worn seats were restored and machined back to original dimensions. Client: Estonia.
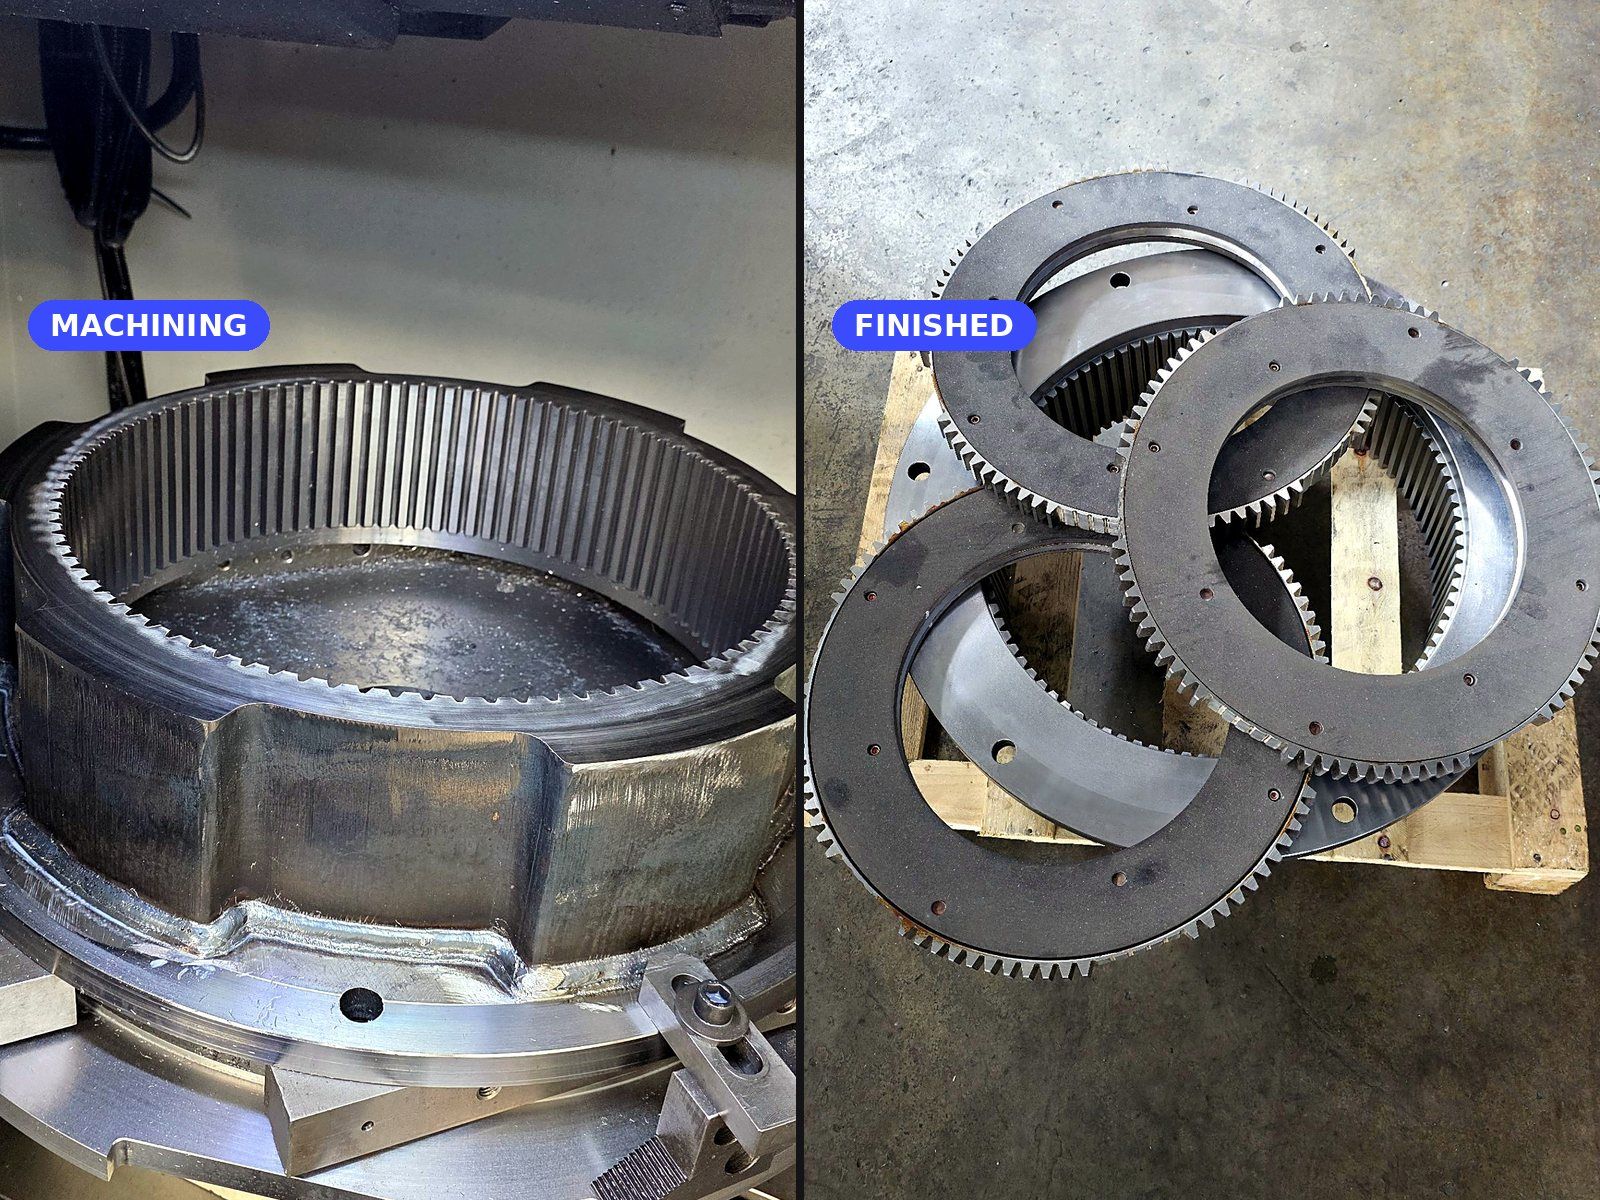
The clutch baskets were manufactured and fully machined in our workshop, including the internal gear teeth. Client: Estonia.
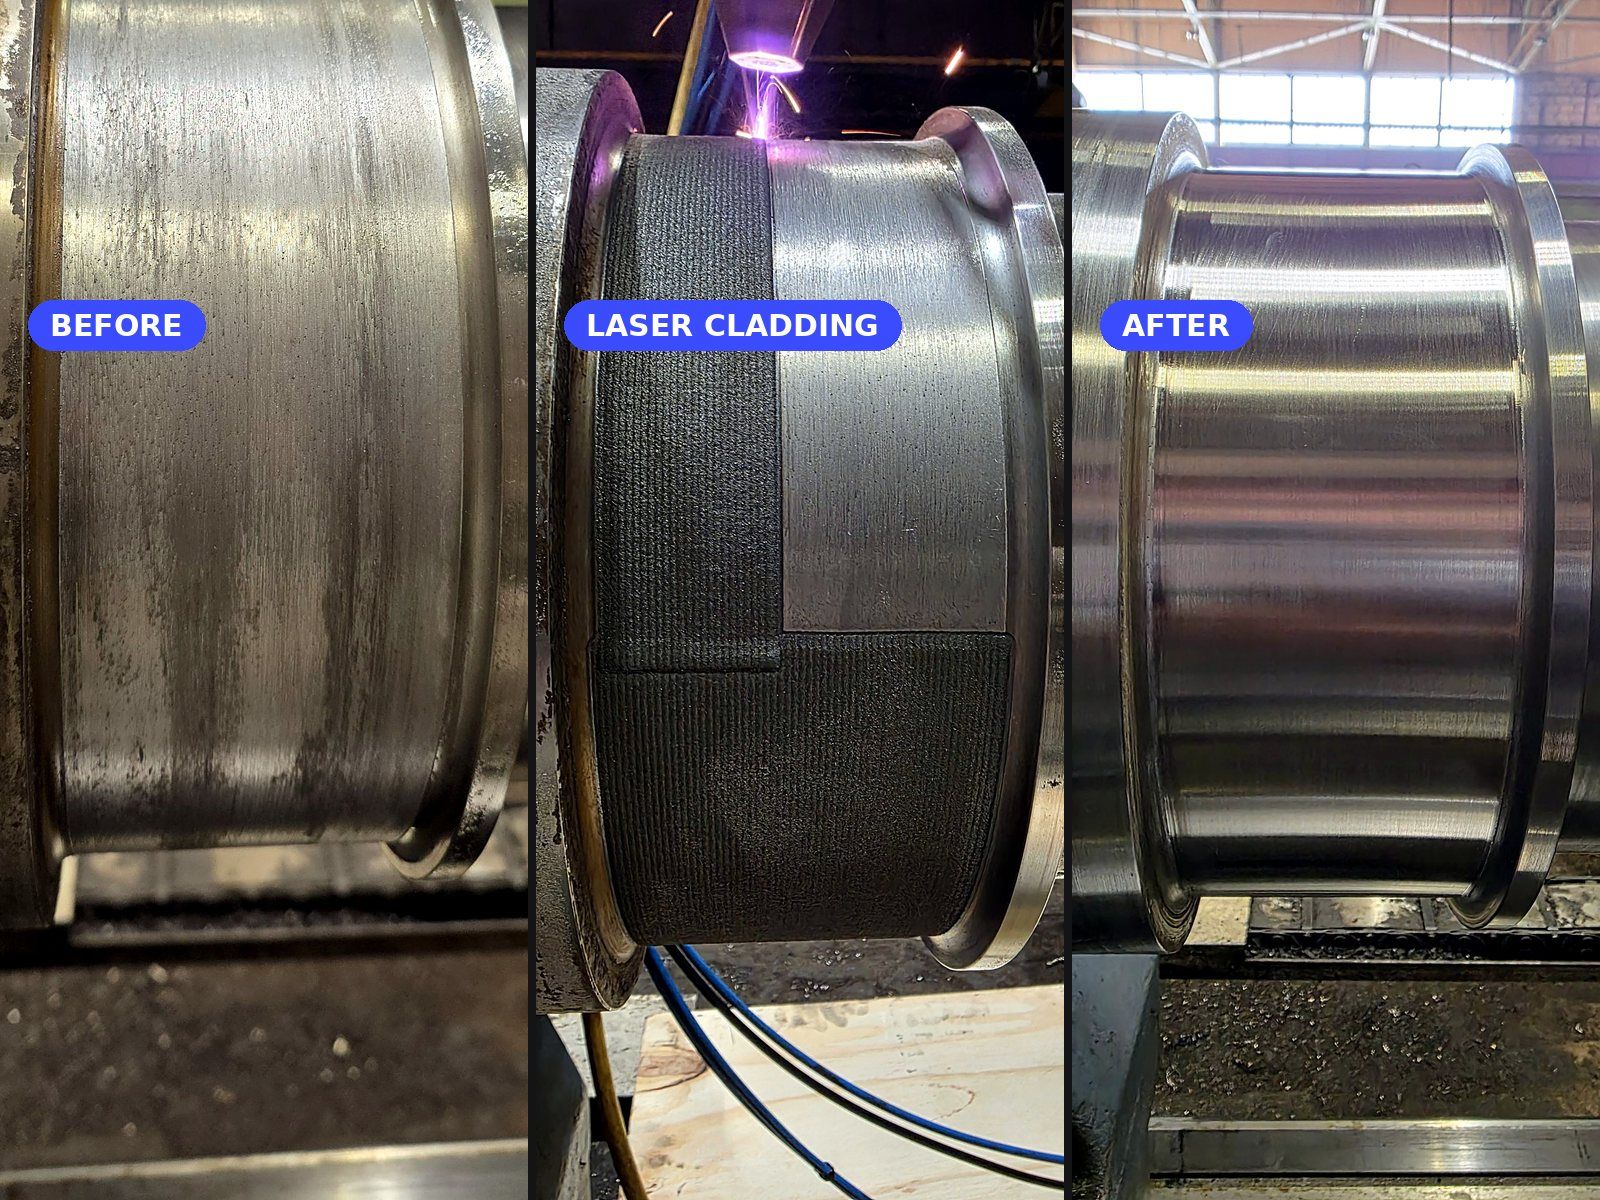
We brought our robotic laser cladding equipment to the customer’s facility and restored the journal there, so the rotor never had to be transported to a workshop. The worn journal was built up by laser cladding and machined back to its original dimensions. Client: Estonia.
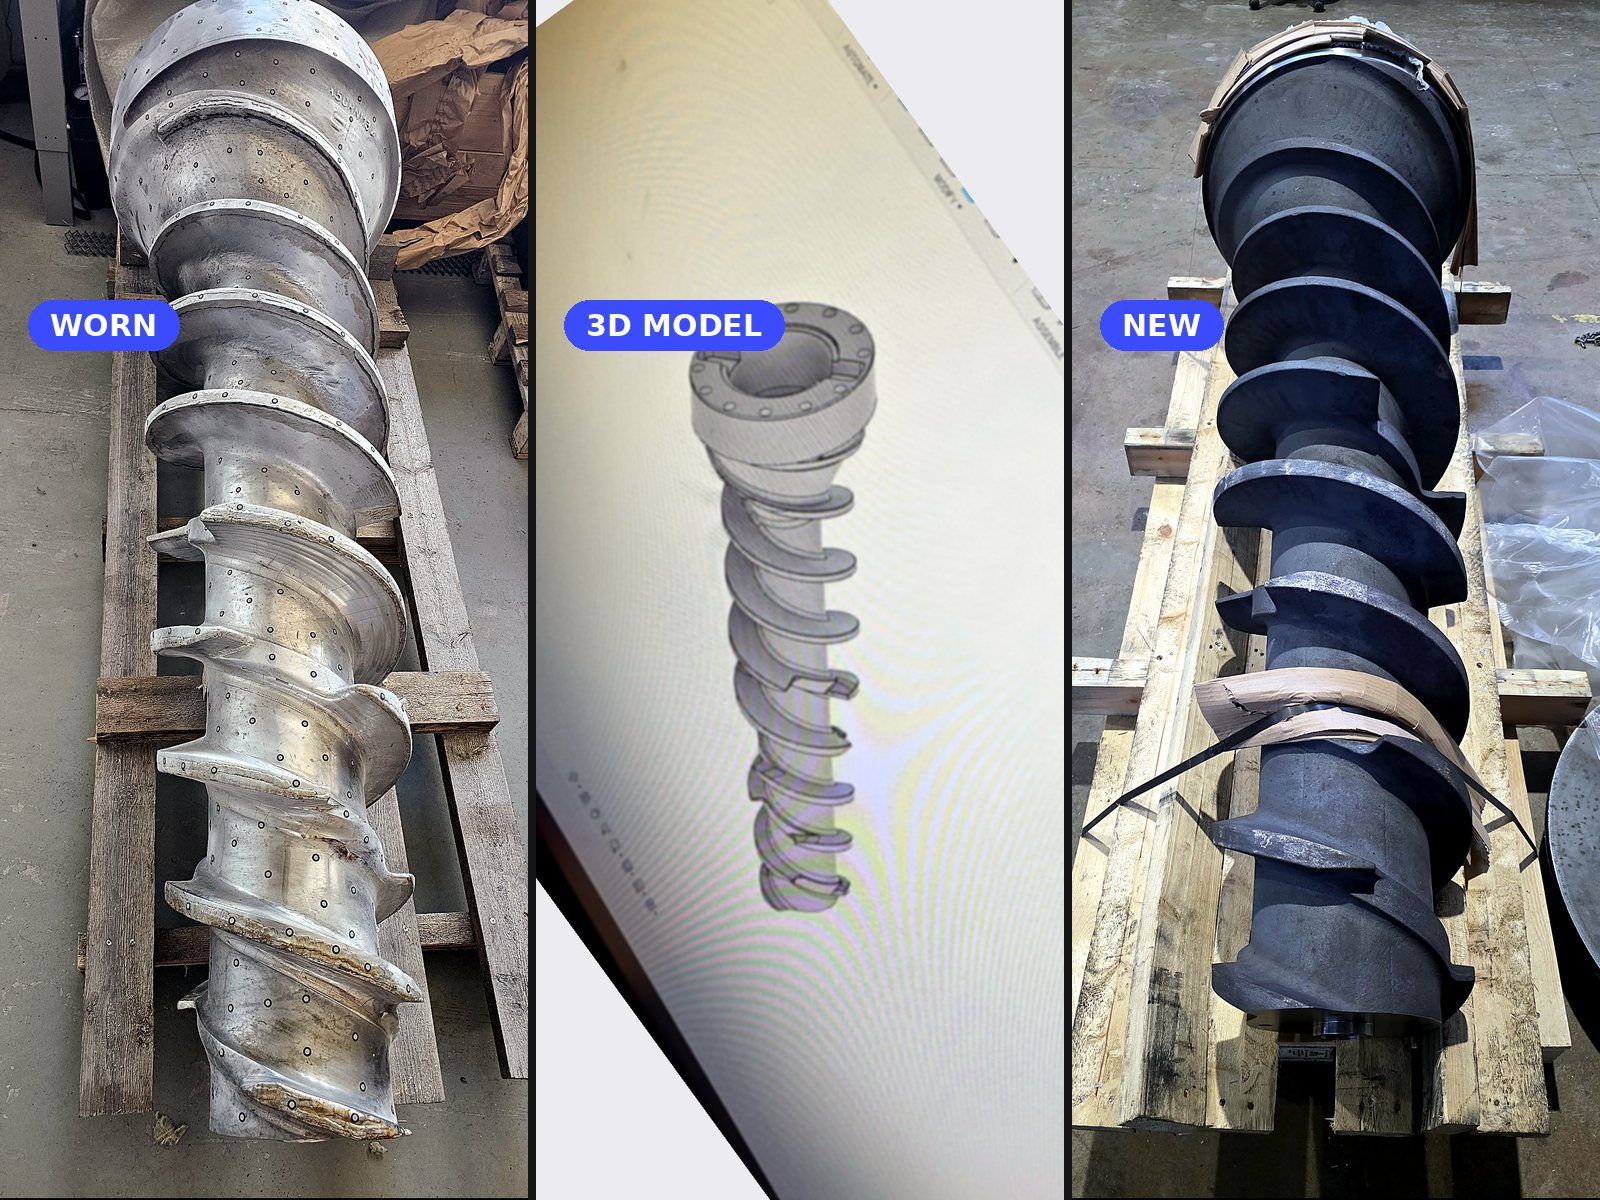
The pulp mill brought us the worn screw to assess whether a new one could be made. We 3D-scanned it, rebuilt the full geometry as a CAD model and manufactured a new screw — 40% cheaper than the original spare part and with improved properties. Client: Estonia.
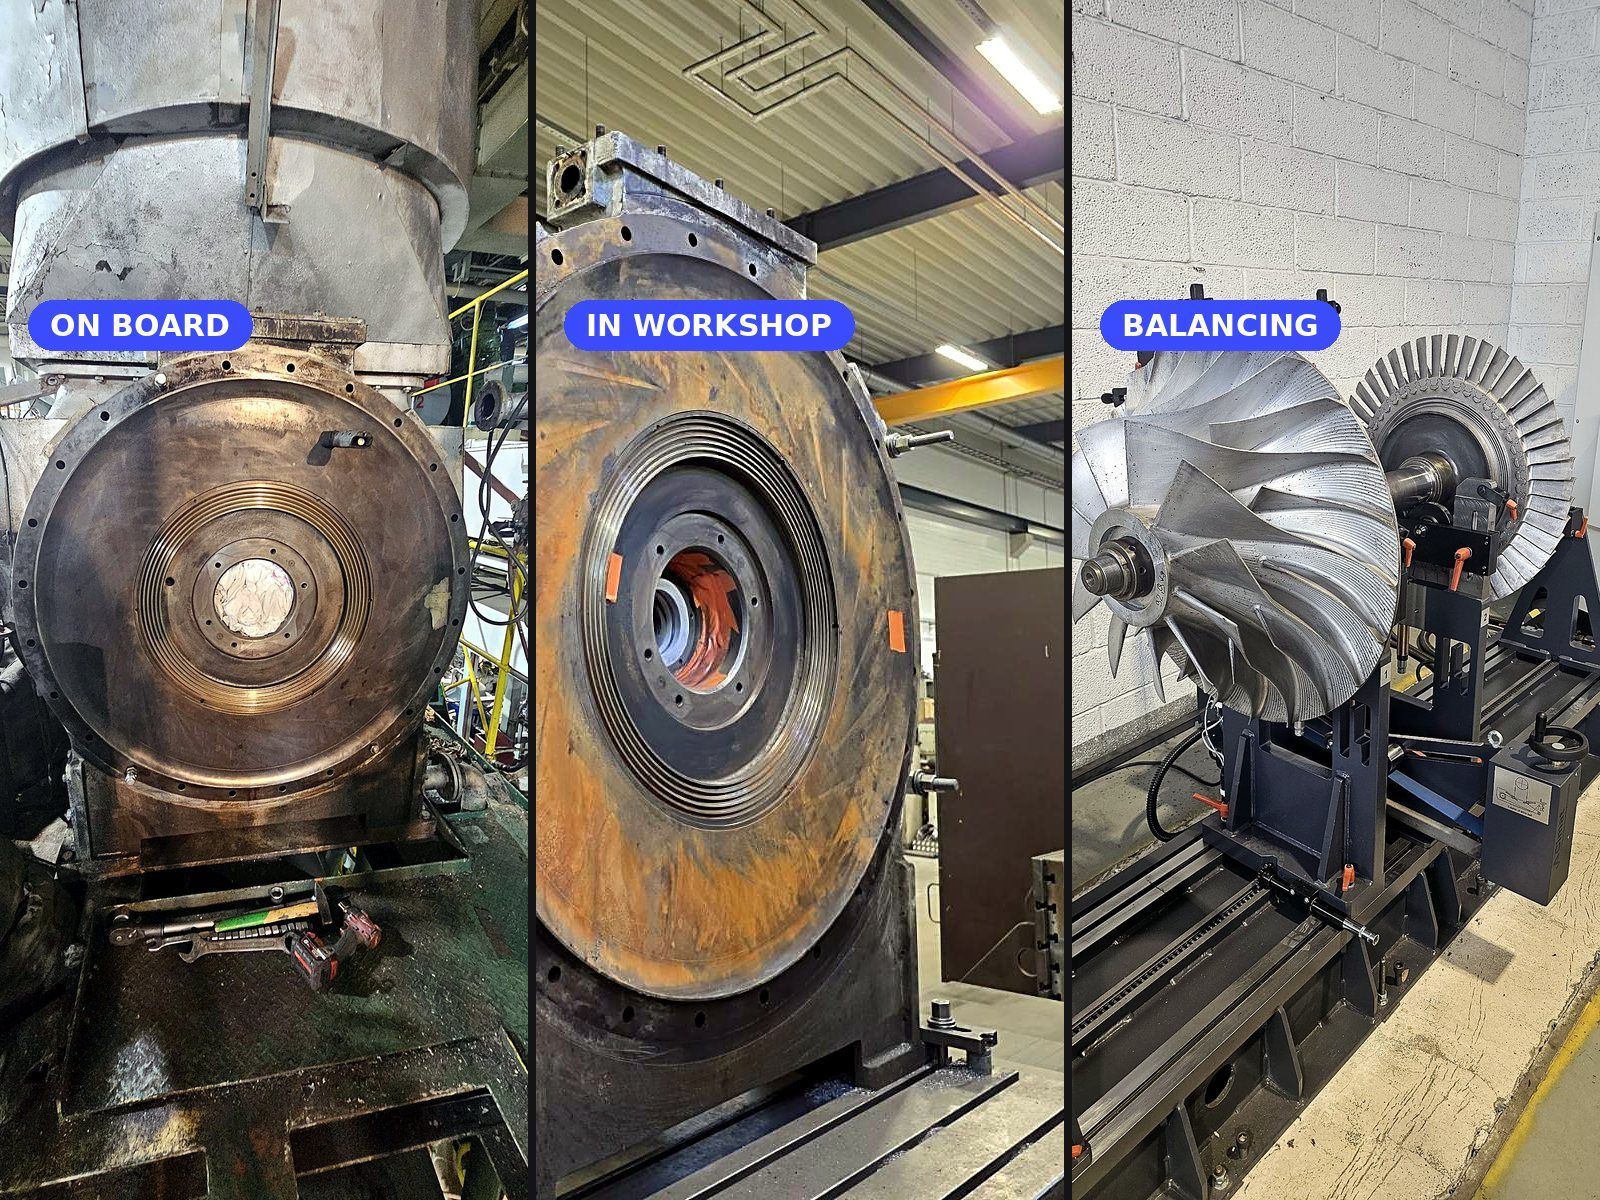
Our team dismantled the turbocharger and removed it from the ship. In the workshop we restored the casing geometry by machining, repaired the rotor, 3D-scanned it and balanced it. Client: Germany.
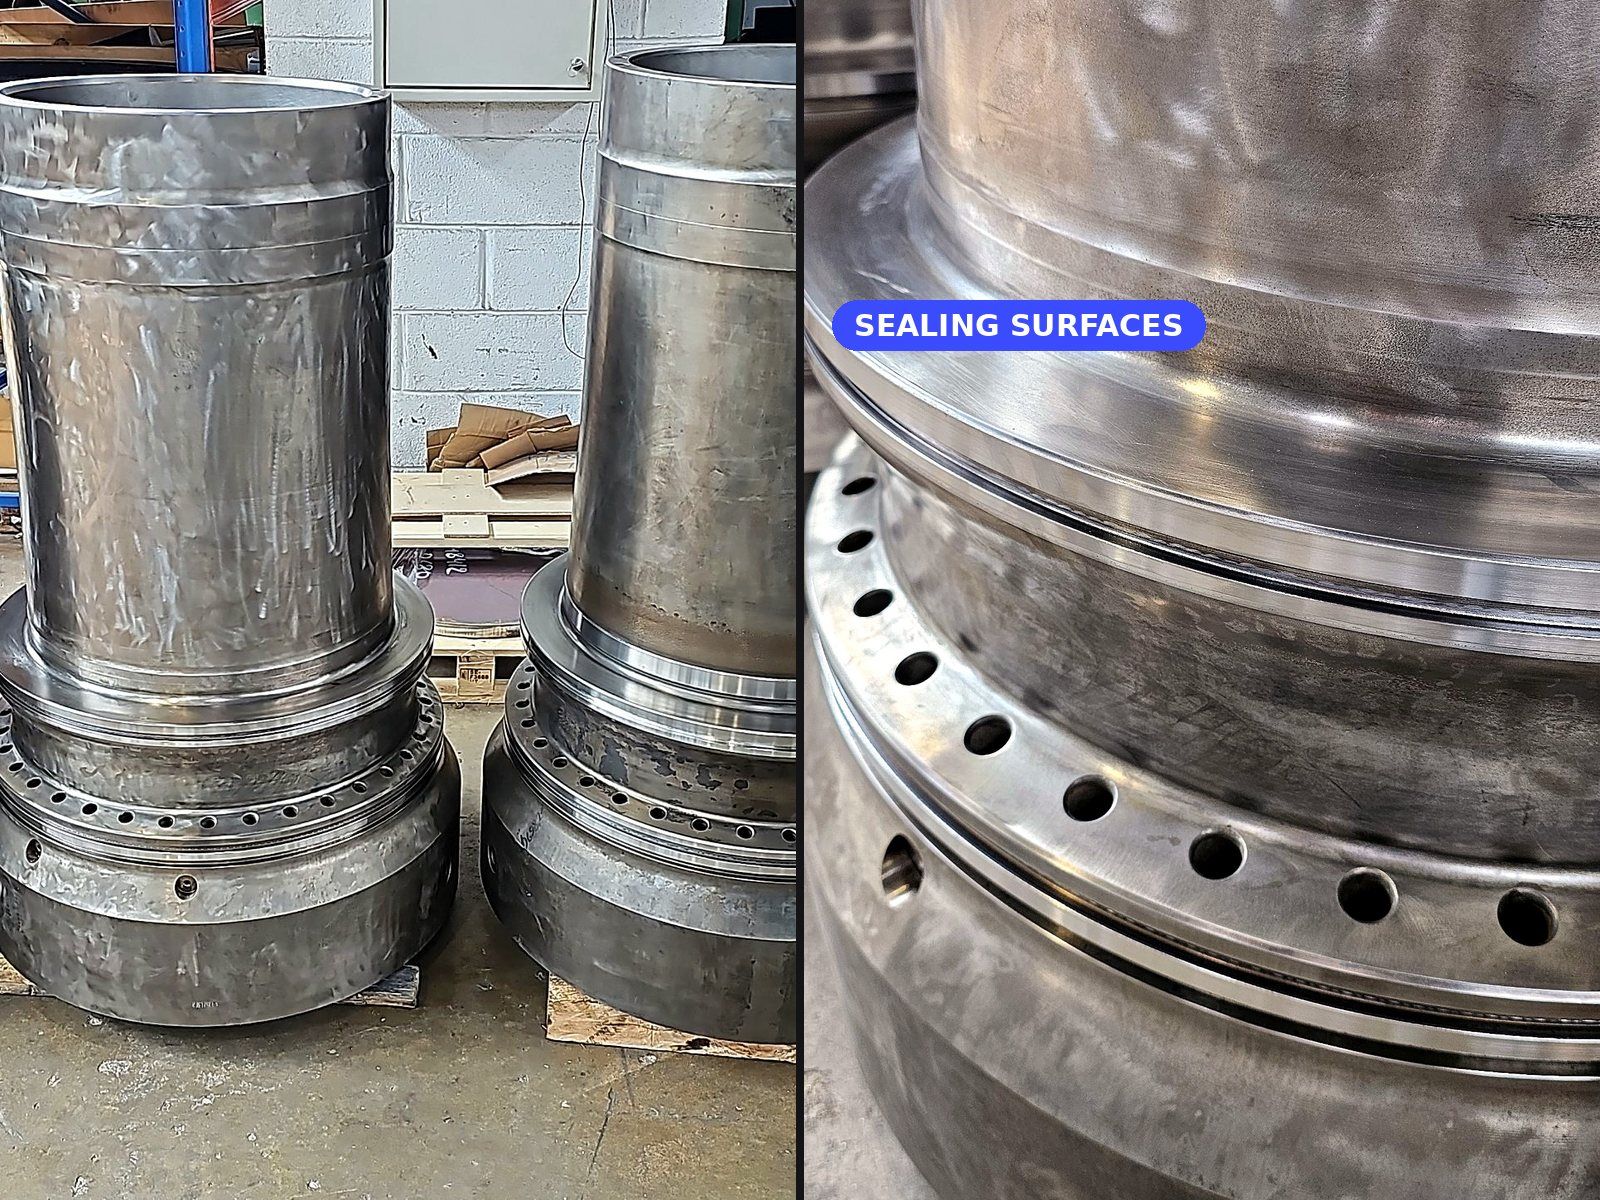
The liners had damaged sealing surfaces and were destined for scrap. We restored the sealing surfaces and returned all seven to service, saving the customer around €50k compared with new liners. Client: Netherlands.
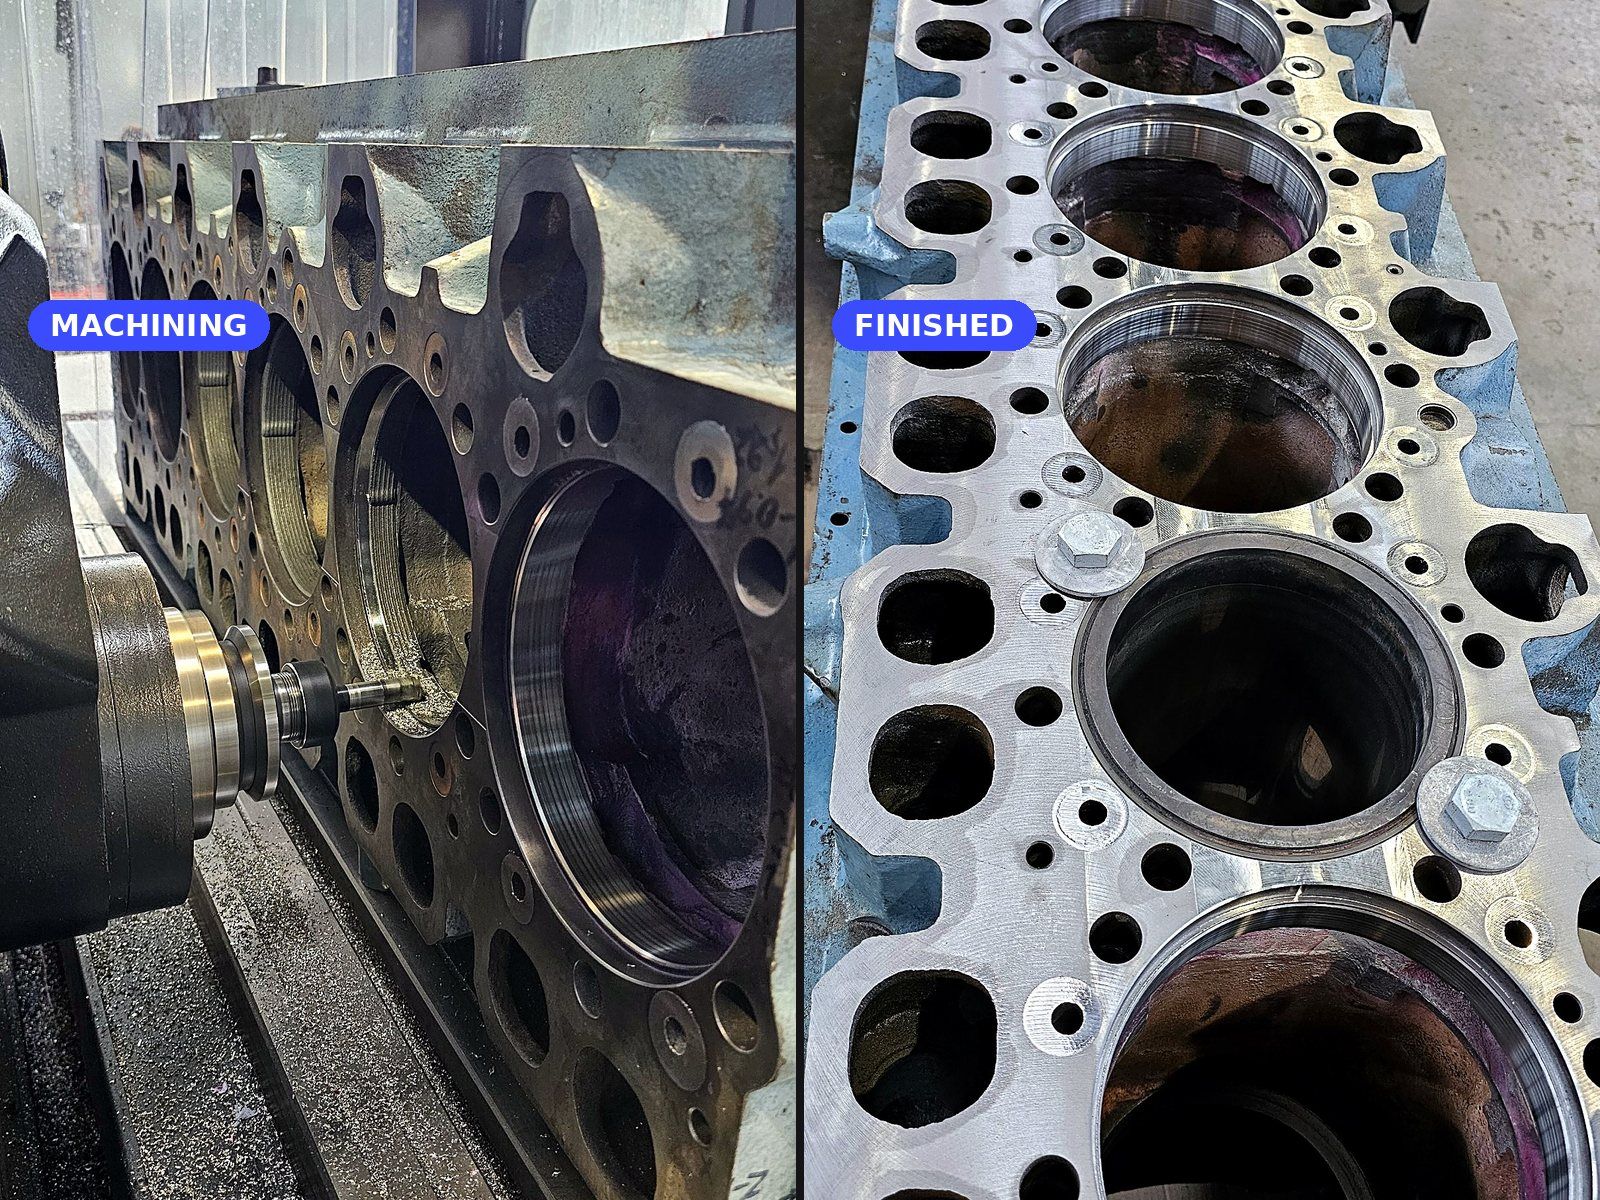
The damaged areas were laser clad with 316L stainless steel and machined back to original dimensions. Unlike a repair in the base material, the stainless layer resists corrosion and cavitation, so the damage does not return. The low heat input of laser cladding avoids distortion and cracking of the block, and the metallurgical bond will not peel off like sprayed or polymer repairs. Client: Netherlands.
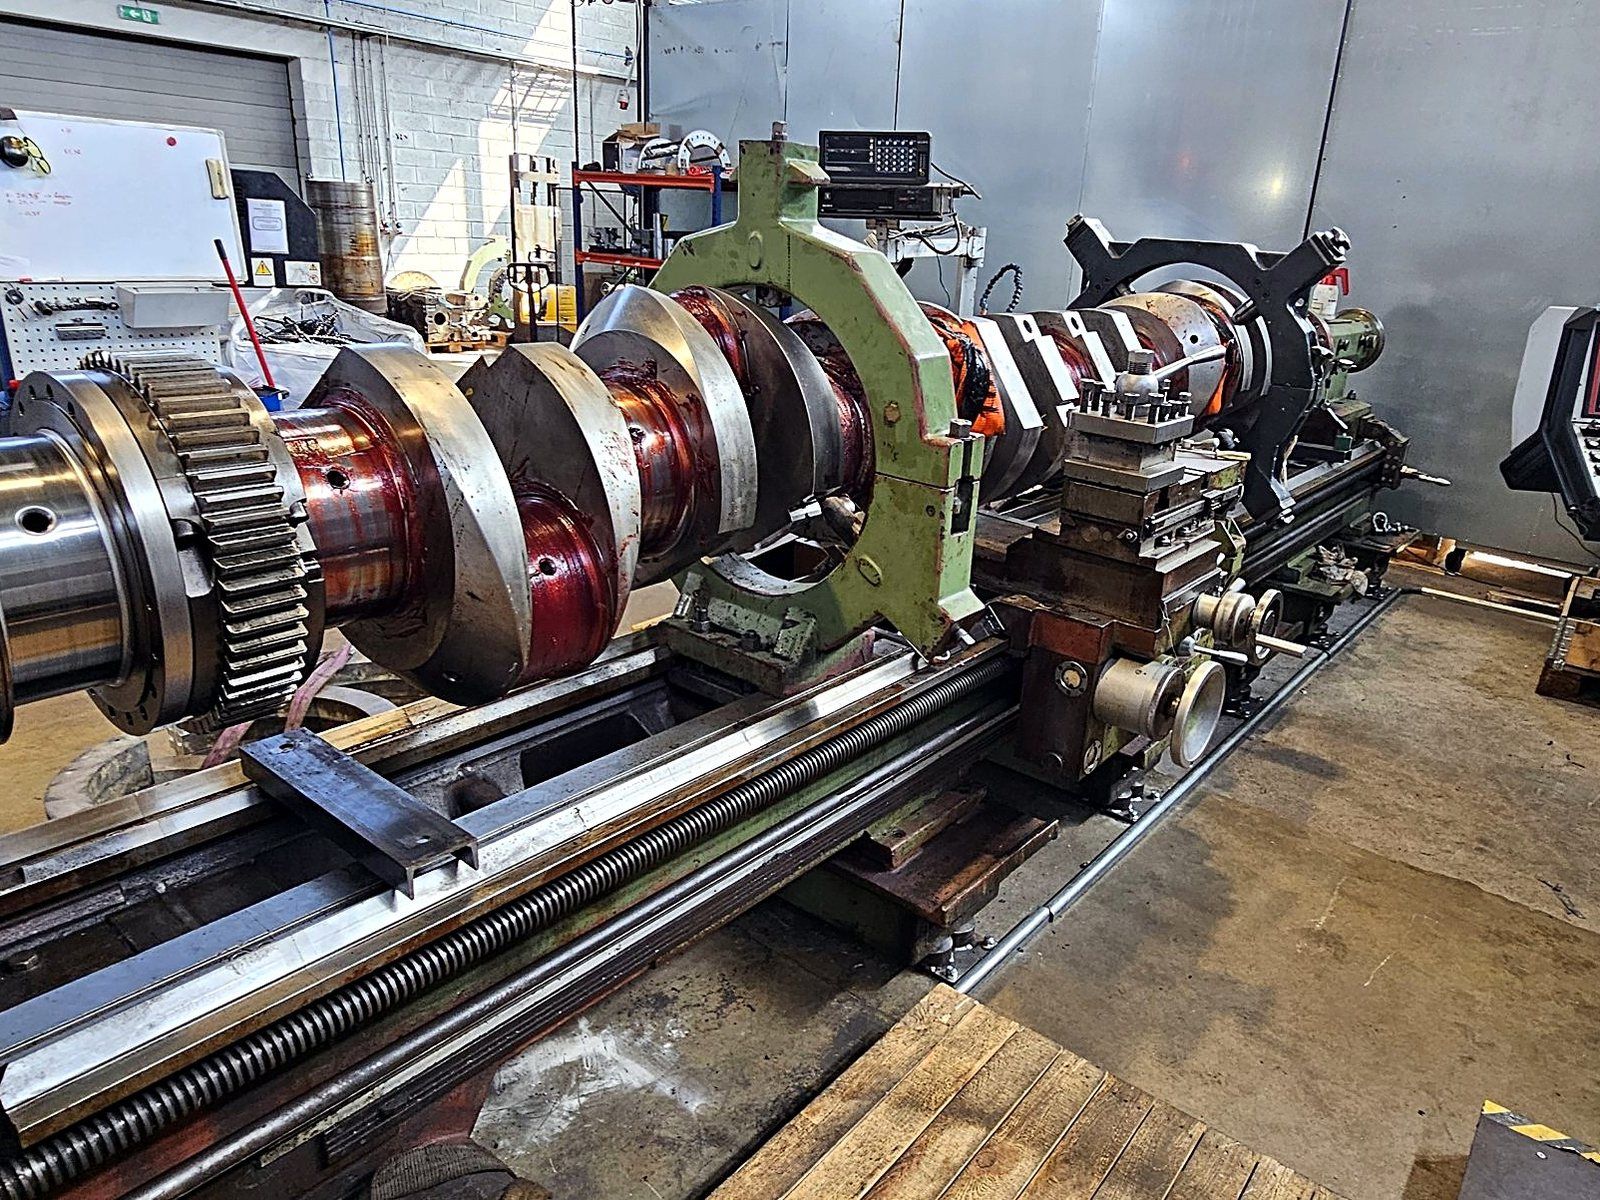
The crankshaft was mounted on our large lathe and checked for runout journal by journal to determine whether a journal was bent, giving the customer a clear basis for the repair decision. Client: Denmark.
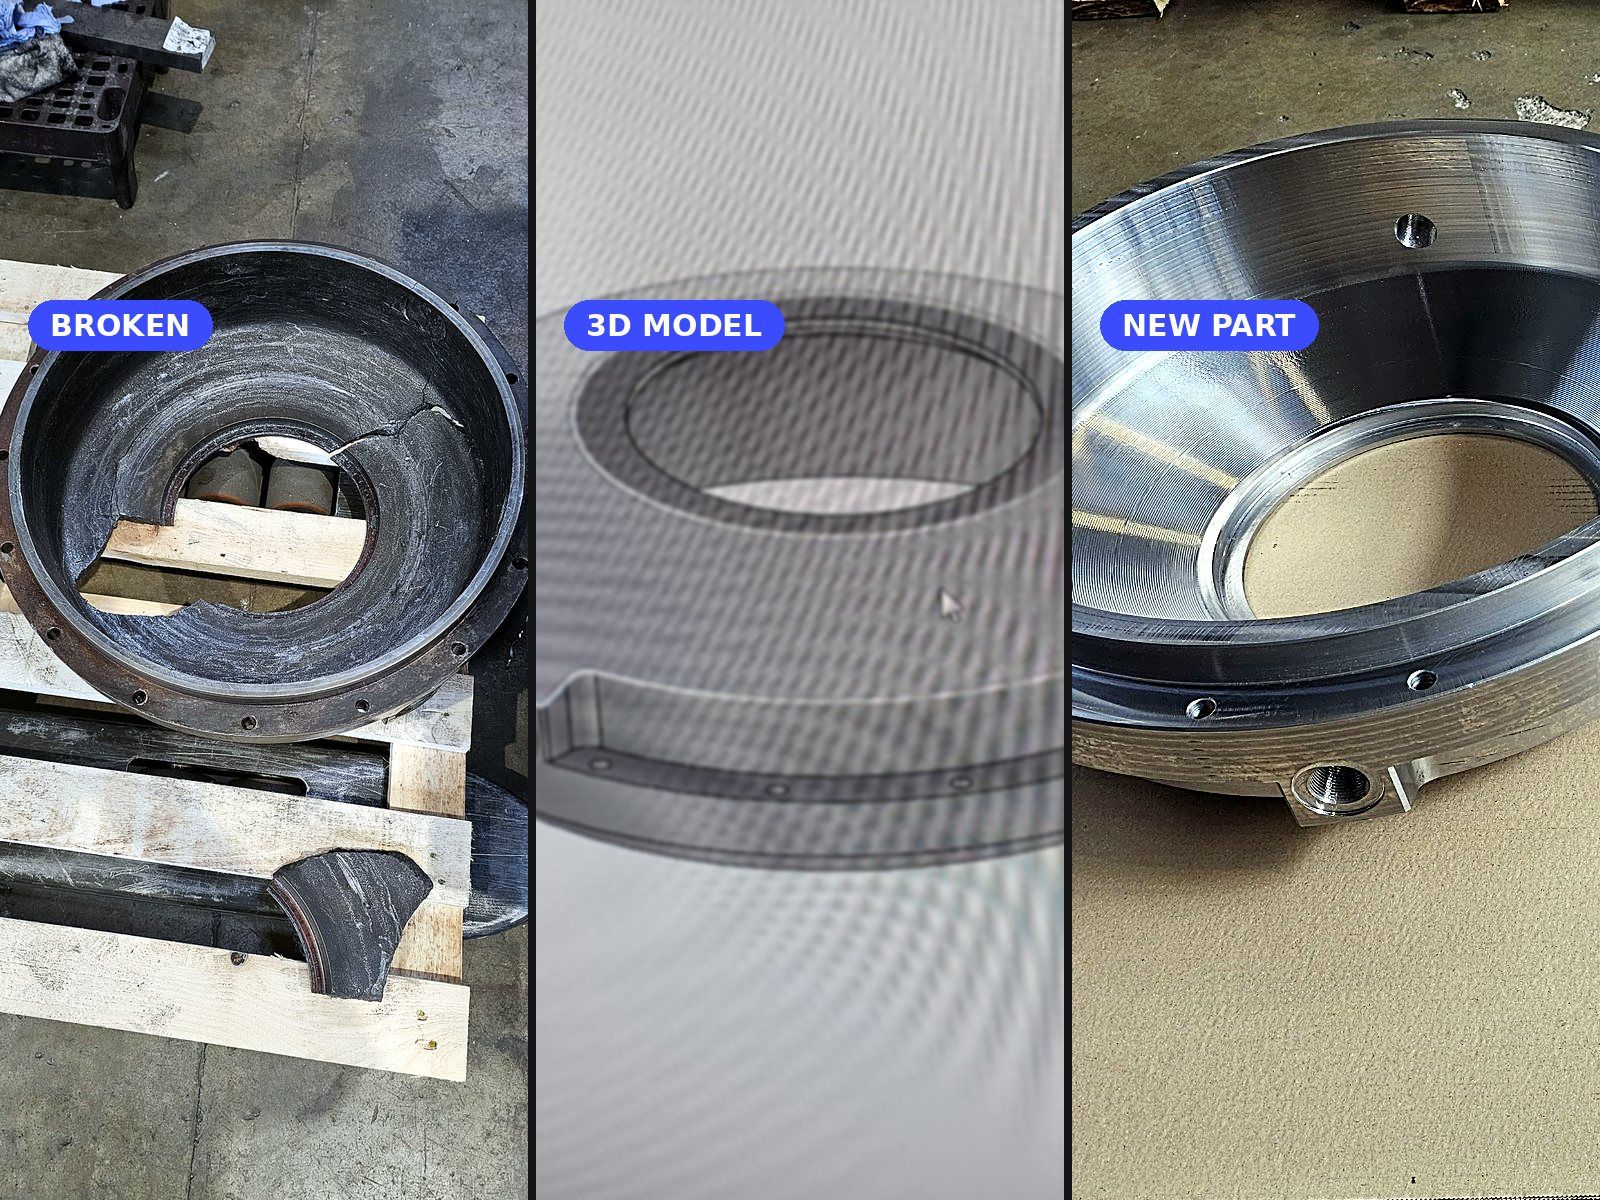
The cast bearing cover of a gearbox cracked and broke apart, and the customer’s whole production was standing because of this one part. We 3D-scanned the broken cover, rebuilt the CAD model and manufactured a new cover in 3 days. Client: Estonia.
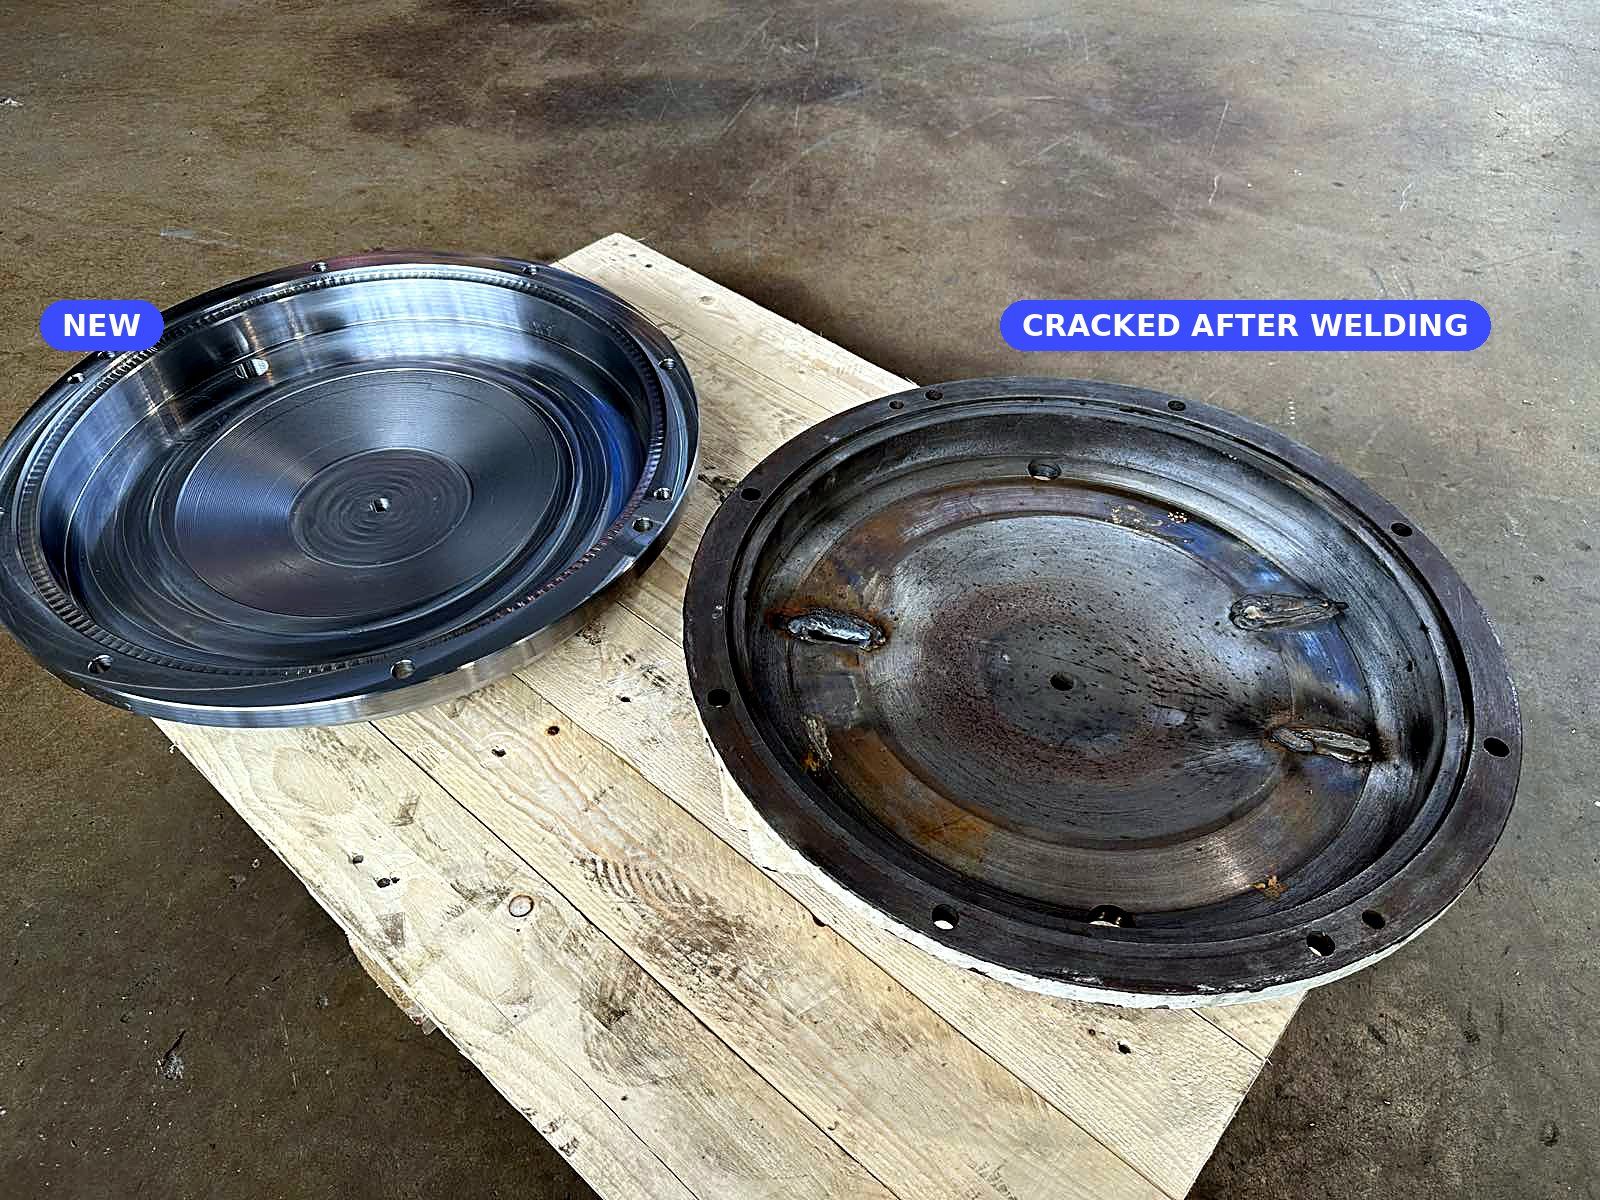
The end cover of an electric motor also works as the brake disc on its back side. After an unsuccessful welding repair attempt it cracked and was brought to us. We measured the part and manufactured a complete new cover in 2 days. Client: Estonia.
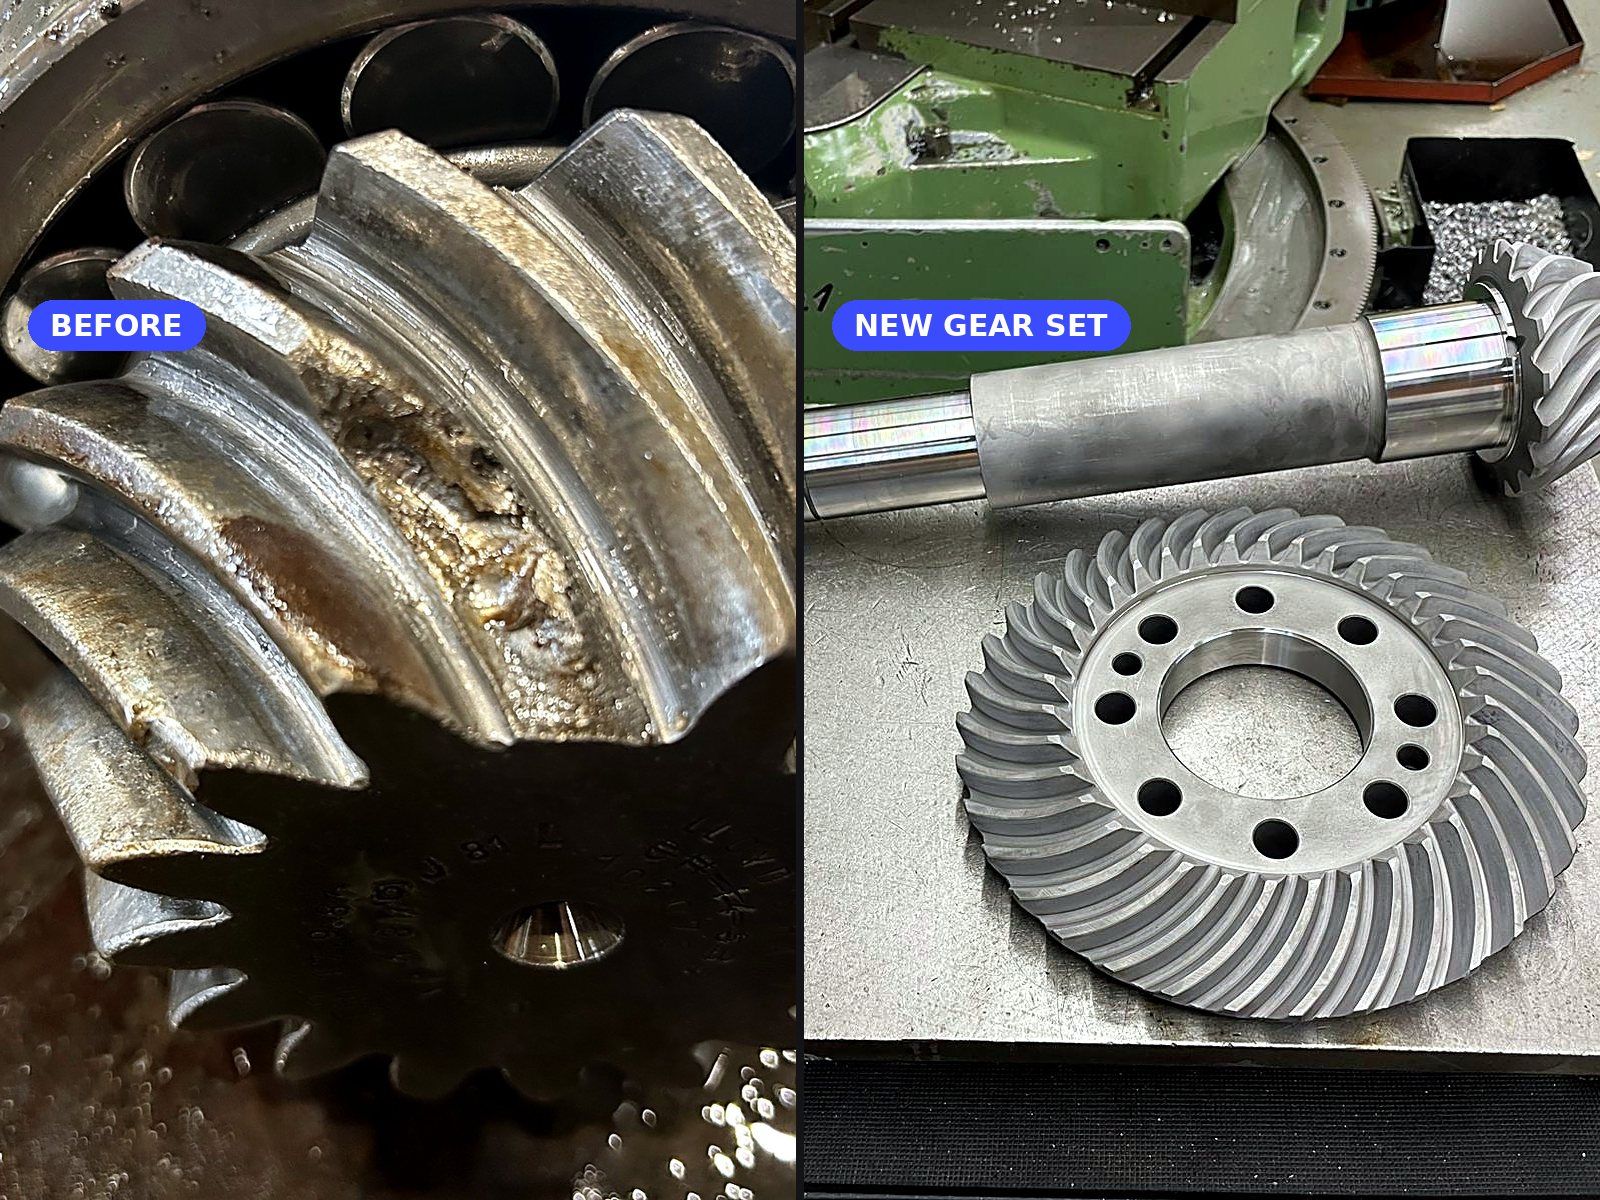
Both the pinion shaft and the crown wheel had broken and spalled teeth. We manufactured a complete new spiral bevel gear set in our workshop. Client: Estonia.
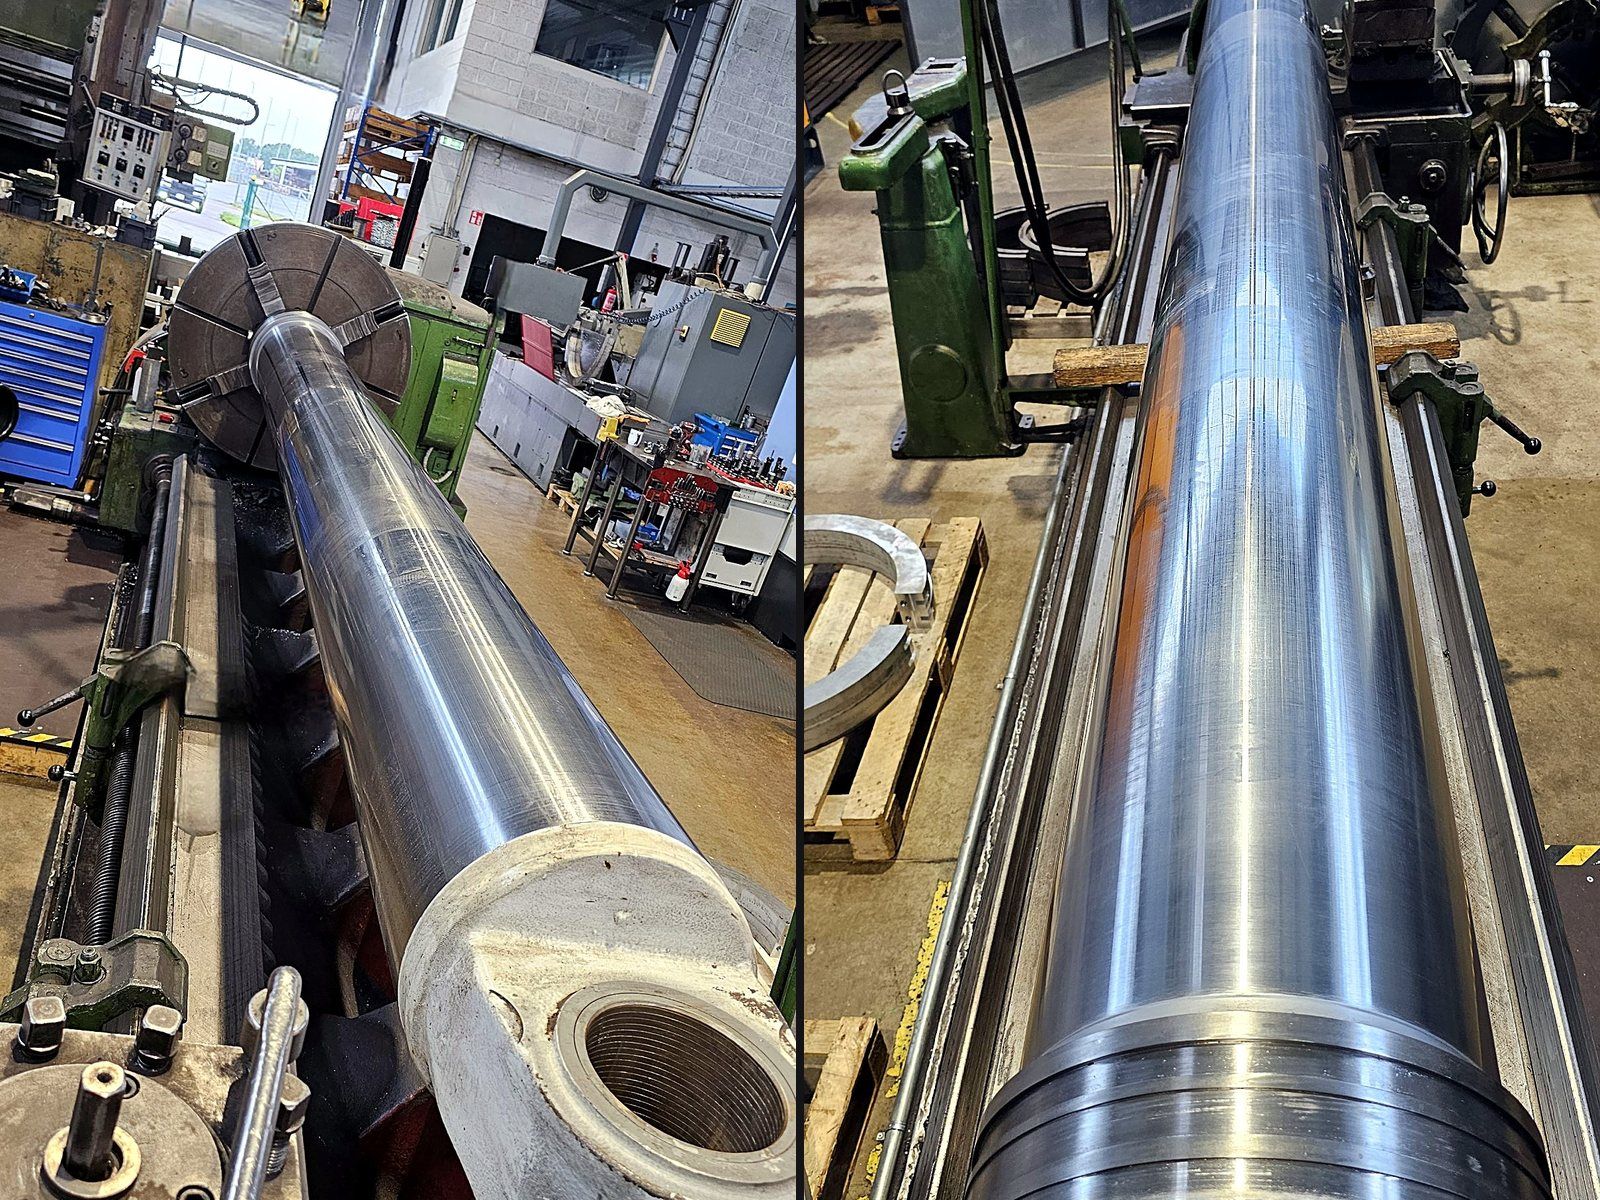
We repair and manufacture hydraulic cylinders and piston rods up to 400 mm in diameter and 4800 mm in length. Client: Finland.

Production Stopped?
We turn around critical parts in 24–48 hours. No delays. No excuses.