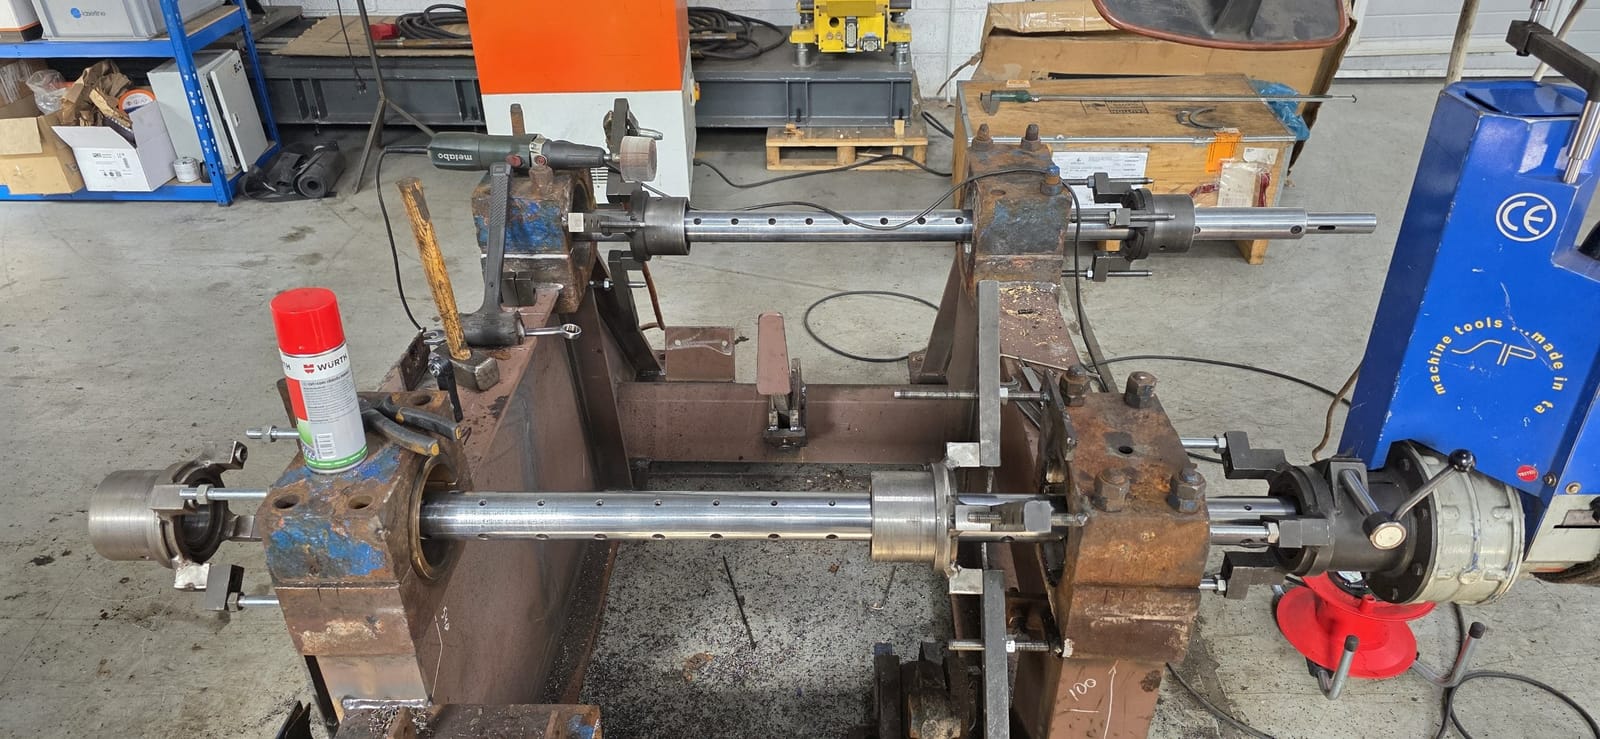
Bearing Seat Repair
Worn or oval bearing seats, misaligned bores and damaged sealing faces are built up and machined back to original geometry — in our workshop in Tallinn, or on site when the housing cannot be removed.
Typical housing problems
How a bearing seat repair runs
Photos and dimensions
Send photos of the damage, a drawing or basic dimensions. Initial technical feedback usually within one business day.
Measurement
Bores are measured for wear, ovality and alignment.
Build-up
Worn areas are built up by laser cladding or welding.
Machining
Boring, line boring or milling back to original geometry.
Capabilities
- On-site milling
- Portable milling equipment, set up with a dial indicator →
- Laser cladding
- 316L, Inconel, Stellite, hard alloys →
- Brush plating (nickel)
- Small surfaces and minor wear, as an alternative to laser cladding
Bearing seats and housings: completed works
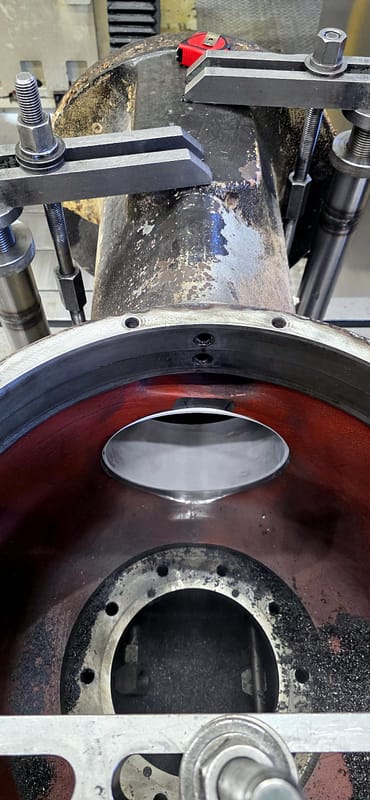
Thruster housing
Worn bearing seat and lost geometry in a thruster housing
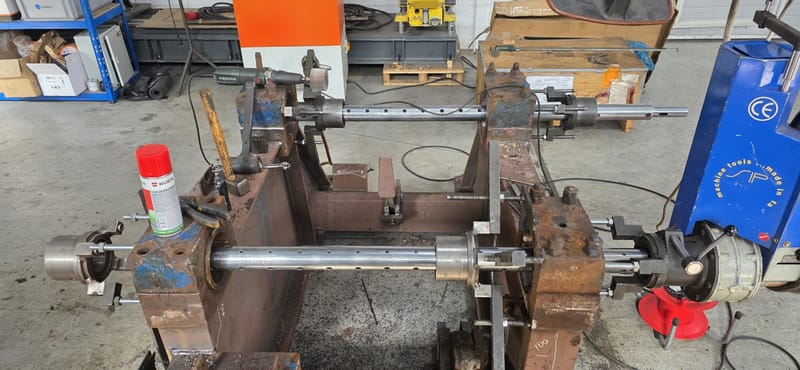
Winch housing
Worn and misaligned bores in a winch housing — two shaft axes out of line
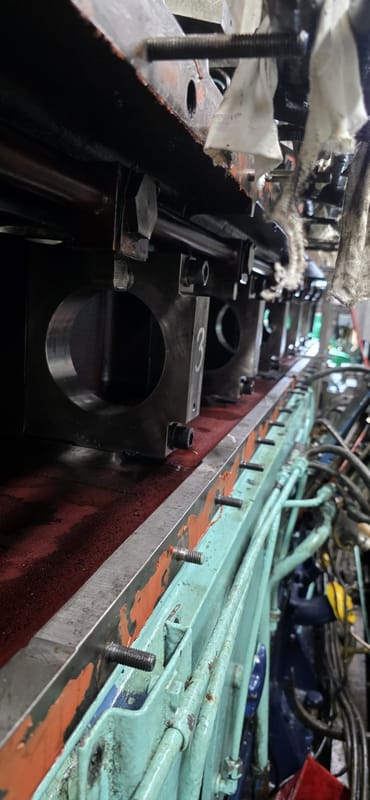
Camshaft bearing housing seat
A broken camshaft damaged the camshaft bearing housing seat in the engine block
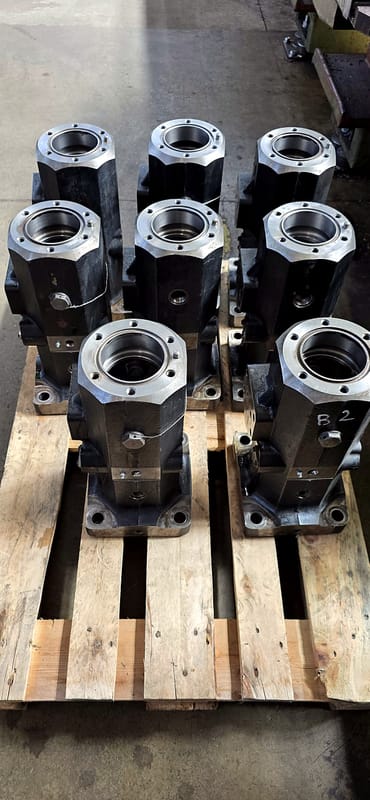
Fuel pump housings
Worn seats in fuel injection pump housings
8 Housings restored
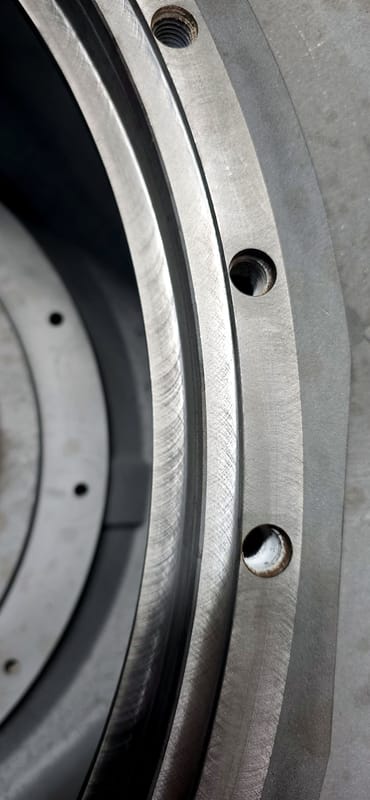
ABB turbocharger casing
ABB turbocharger casing with worn surfaces and lost geometry
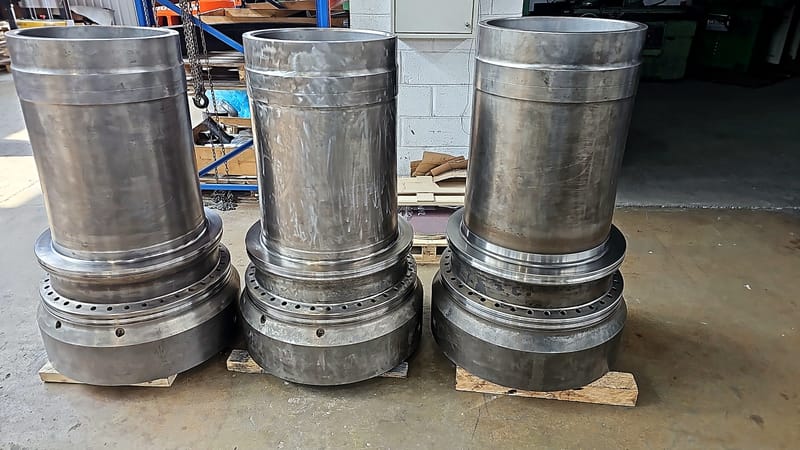
Wärtsilä 46 cylinder liners
Seven Wärtsilä 46 cylinder liners written off as scrap
7 Liners saved from scrap
Send us the problem
Photos of the damage, a drawing or basic dimensions and information about where the component is installed are enough to start.
Initial technical feedback usually within one business day.